SNDB Acetic Acid Solutions for Pharmaceuticals, Textiles, and Chemical IndustriesCategoriesAcid

Top Acetic Acid Manufacturer and Global Exporter | SNDB

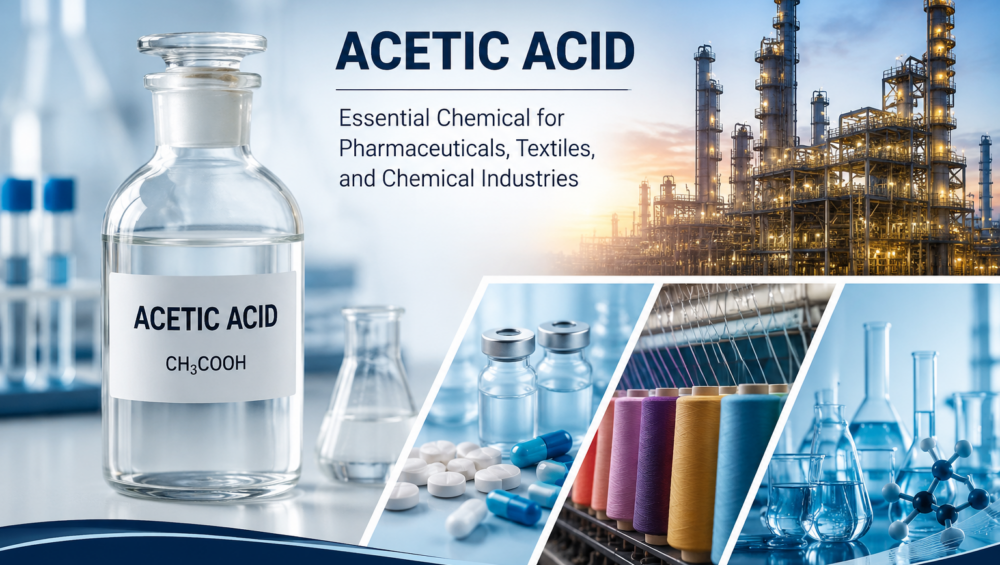
Acetic acid is one of the most widely used industrial chemicals, playing a vital role in the production of pharmaceuticals, textiles, food processing, paints, adhesives, plastics, and various specialty chemicals. Choosing a trusted manufacturer and exporter ensures consistent quality, timely delivery, and reliable support. SNDB has earned a strong reputation as a leading acetic acid manufacturer and global exporter by delivering premium-grade chemical solutions that meet international quality standards. With years of industry expertise, advanced manufacturing processes, and a customer-centric approach, SNDB has become the preferred partner for businesses worldwide seeking high-purity acetic acid.

Premium Quality Acetic Acid for Diverse Industries

SNDB manufactures high-quality acetic acid designed to meet the needs of multiple industries. Every batch is produced under strict quality control measures to ensure exceptional purity, consistency, and performance. Whether you require acetic acid for chemical manufacturing, pharmaceuticals, textiles, food processing, or laboratory applications, SNDB delivers products that comply with international specifications. The company’s commitment to quality enables customers to achieve better production efficiency while maintaining safety and reliability in their operations.

Wide Applications of Acetic Acid

Acetic acid is a versatile chemical with numerous industrial applications. It is widely used in the production of vinyl acetate monomer, purified terephthalic acid, acetate esters, and acetic anhydride. It also plays a significant role in the textile and dyeing industry, pharmaceutical manufacturing, food preservation, and chemical synthesis. Due to its excellent chemical properties, acetic acid is an essential raw material for industries requiring high-performance chemical solutions. SNDB supplies premium acetic acid suitable for both industrial-scale manufacturing and specialized applications.

Why Choose SNDB as Your Acetic Acid Supplier?

SNDB is recognized for delivering superior-quality acetic acid backed by exceptional customer service. The company focuses on maintaining international quality standards, competitive pricing, and efficient logistics to ensure seamless supply worldwide. Every order is handled with precision, from manufacturing and quality testing to secure packaging and timely shipment. Customers trust SNDB because of its consistent product quality, transparent business practices, and commitment to long-term partnerships. These strengths make SNDB a preferred supplier for businesses seeking dependable chemical solutions.

Global Export Network with Reliable Supply

As a trusted global exporter, SNDB serves customers across multiple countries with efficient and dependable supply chain management. The company understands the importance of timely deliveries and secure packaging for international shipments. By adhering to global export standards and maintaining a robust distribution network, SNDB ensures that customers receive high-quality acetic acid without delays. Whether supplying bulk industrial orders or customized packaging solutions, the company delivers reliable service that meets the expectations of clients around the world.

Partner with SNDB for High-Quality Acetic Acid

When selecting an acetic acid manufacturer and exporter, quality, consistency, and reliability are essential. SNDB combines advanced manufacturing capabilities, strict quality assurance, competitive pricing, and global distribution expertise to provide customers with the best chemical solutions. Businesses across various industries rely on SNDB for premium acetic acid that supports efficient production and long-term success. If you are looking for a trusted partner for high-quality acetic acid supply, SNDB is committed to delivering excellence with every shipment.
SNDB: Best Manufacturer, Supplier, and Exporter of Hydrogen PeroxideCategoriesHydrogen Peroxide

SNDB | Hydrogen Peroxide: Environmental and Industrial Applications

Hydrogen Peroxide (H₂O₂) is a widely used chemical known for its powerful oxidizing properties. It plays an important role in both environmental protection and industrial processes. Because it breaks down into water and oxygen, it is often considered an environmentally friendly alternative to more harmful chemicals.

Environmental Applications

One of the most important environmental uses of hydrogen peroxide is in water and wastewater treatment. It helps remove pollutants, eliminate unpleasant odors, and reduce the presence of harmful organic compounds. Because it decomposes into harmless by-products, it supports cleaner and safer water treatment processes.

Hydrogen peroxide is also used in soil remediation. Contaminated soil can be treated with controlled doses of hydrogen peroxide to break down pollutants such as petroleum hydrocarbons. This helps restore soil quality without introducing toxic residues.

In addition, hydrogen peroxide plays a role in air pollution control. Industries use it to help neutralize harmful gases and odors, contributing to cleaner air emissions.

Industrial Applications

In industrial settings, hydrogen peroxide is used in a wide range of processes:

Pulp and Paper Industry: It is commonly used as a bleaching agent in paper production, helping to whiten paper without relying on chlorine-based chemicals. This reduces harmful environmental impacts.

Textile Industry: Hydrogen peroxide is used to bleach fabrics, especially cotton, to achieve brighter and cleaner textiles in an eco-friendly way.

Chemical Manufacturing: It serves as a key ingredient in producing other chemicals, such as peroxides and oxidizing agents. It also plays a role in various synthesis reactions.

Electronics Industry: Hydrogen peroxide is used for cleaning and etching electronic components, including semiconductors and circuit boards, due to its strong oxidizing properties.

Food Industry: It is sometimes used for sterilization of packaging materials and surfaces in food processing environments to maintain hygiene standards.

Advantages of Using Hydrogen Peroxide

Hydrogen peroxide is valued for its environmentally friendly profile. Unlike many traditional chemicals, it decomposes into water and oxygen, reducing the risk of harmful residues. Its effectiveness at low concentrations makes it both economical and environmentally responsible.

Safety Considerations

Although hydrogen peroxide is considered safer than many industrial chemicals, it must still be handled carefully. Concentrated solutions can cause skin and eye irritation, and improper storage may lead to decomposition or pressure buildup. Proper handling procedures are necessary in both industrial and household use.

Hydrogen peroxide is an important chemical with a wide range of environmental and industrial applications. Its strong oxidizing properties, combined with its environmentally friendly decomposition, make it a valuable tool in water treatment, pollution control, manufacturing, and many other fields. When used responsibly, hydrogen peroxide supports cleaner production processes and environmental protection.

SNDB has emerged as one of the best manufacturers, suppliers, and exporters of hydrogen peroxide due to its commitment to quality, innovation, and sustainability. With a wide product range, global presence, and customer-focused services, the company continues to play a significant role in the chemical industry.

As demand for eco-friendly and efficient chemicals grows, SNDB remains a reliable partner for industries seeking high-quality hydrogen peroxide solutions.

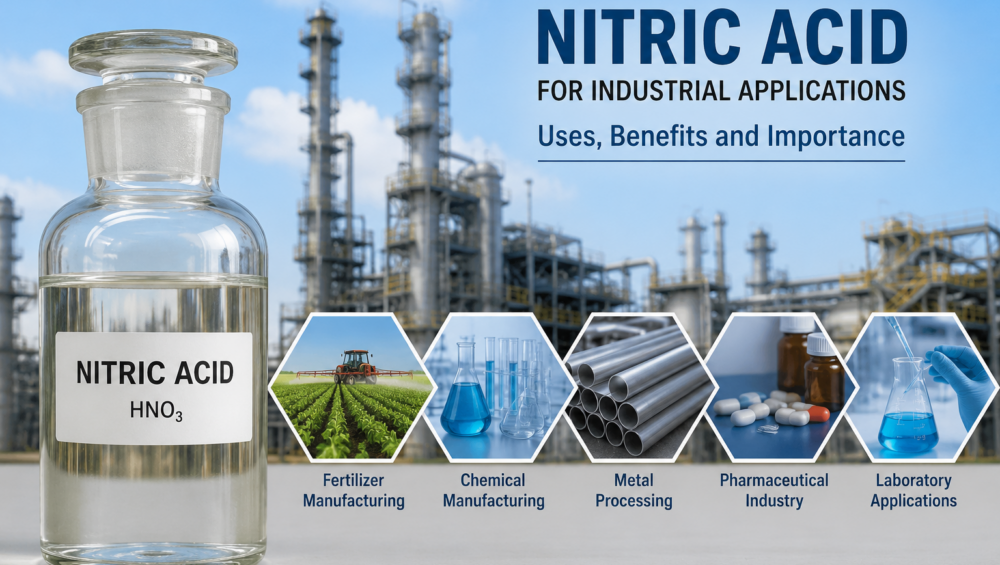
Nitric Acid for Industrial Applications: Uses, Benefits and Importance | SNDBCategoriesNitric Acid

Nitric Acid for Industrial Applications: Uses, Benefits and Importance | SNDB

Nitric acid is an important industrial chemical widely used in fertilizer production, chemical manufacturing, metal processing, pharmaceuticals, and several other industries. Due to its strong chemical properties and versatility, nitric acid plays an essential role in many industrial processes.

SNDB is a trusted manufacturer and supplier of industrial chemicals, offering quality nitric acid solutions for various industrial requirements. With a focus on consistent quality and reliable supply, SNDB supports businesses across different sectors.

What Is Nitric Acid?

Nitric acid is a strong mineral acid with the chemical formula HNO₃. It is a clear to slightly yellow liquid and is highly reactive. Nitric acid is known for its strong oxidizing properties and is commonly used as a raw material and processing agent in the chemical industry.

Its chemical characteristics make it suitable for applications where nitration, oxidation, and chemical processing are required.

Industrial Uses of Nitric Acid

Nitric acid has a wide range of industrial applications. Some of its major uses include:

1. Fertilizer Manufacturing

One of the largest applications of nitric acid is fertilizer production. It is used to manufacture nitrate-based fertilizers, including ammonium nitrate and other nitrogen-containing compounds. These fertilizers provide essential nitrogen to crops and are widely used in agriculture.

2. Chemical Manufacturing

Nitric acid is an important raw material in the production of various chemicals. It is used in nitration and oxidation processes and helps manufacture several nitrate compounds and chemical intermediates.

3. Metal Processing

Nitric acid is used in metal treatment and processing applications. It can help remove impurities and oxides from metal surfaces and is used in processes such as pickling and surface treatment for certain metals and alloys.

4. Pharmaceutical Industry

The pharmaceutical sector uses nitric acid as a chemical reagent in selected manufacturing and laboratory processes. Its controlled chemical properties make it useful for producing and processing certain chemical intermediates.

5. Explosives and Nitration Processes

Nitric acid is used as a nitrating agent in controlled industrial chemical processes. Nitration is an important chemical reaction used to produce various industrial intermediates and specialized chemicals.

6. Laboratory and Research Applications

Nitric acid is also widely used in laboratories for analytical procedures, sample preparation, digestion, and chemical testing. Its strong acidic and oxidizing characteristics make it useful in controlled laboratory environments.

Benefits of Nitric Acid in Industrial Applications

Nitric acid offers several advantages for industrial chemical processing:

  • High chemical reactivity: Its strong acidic and oxidizing properties support a variety of chemical processes.
  • Versatile applications: It can be used across fertilizer, chemical, metal, pharmaceutical, and laboratory industries.
  • Effective processing agent: It is useful for oxidation, nitration, cleaning, and surface-treatment processes.
  • Important chemical intermediate: Nitric acid helps manufacture numerous nitrate-based compounds and industrial chemicals.
  • Wide industrial demand: Its applications across multiple sectors make it an important industrial raw material.

Why Quality Nitric Acid Matters

Industrial processes require chemicals with consistent quality and specifications. The purity and appropriate grade of nitric acid can influence process efficiency, product quality, and overall manufacturing performance.

For this reason, industries should source nitric acid from a reliable manufacturer and supplier that follows appropriate quality-control practices and provides material suitable for the intended application.

SNDB: Nitric Acid Manufacturer and Supplier

SNDB focuses on supplying industrial chemicals to businesses that require dependable chemical raw materials for their manufacturing and processing operations. As a nitric acid manufacturer and supplier, SNDB aims to provide consistent-quality products and reliable service to industrial customers.

The company serves different industrial requirements and emphasizes quality, supply reliability, and customer support.

Safe Handling of Nitric Acid

Nitric acid is a highly corrosive and reactive chemical and should always be handled by trained personnel using appropriate industrial safety procedures. Proper storage, compatible containers, protective equipment, ventilation, and emergency measures are important when working with nitric acid.

Businesses should always follow the relevant safety data sheet, regulatory requirements, and site-specific handling procedures.

Nitric acid is a valuable industrial chemical with applications across fertilizer manufacturing, chemical processing, metal treatment, pharmaceuticals, laboratories, and other industries. Its strong acidic and oxidizing properties make it suitable for a wide range of controlled industrial processes.

For businesses looking for a dependable nitric acid manufacturer and supplier in India, SNDB provides industrial chemical solutions with an emphasis on quality and reliable supply. Choosing a trusted supplier can help industries maintain consistency and efficiency in their chemical operations.

How the Right Chemical Supplier Can Improve Water Treatment EfficiencyCategoriesAcid

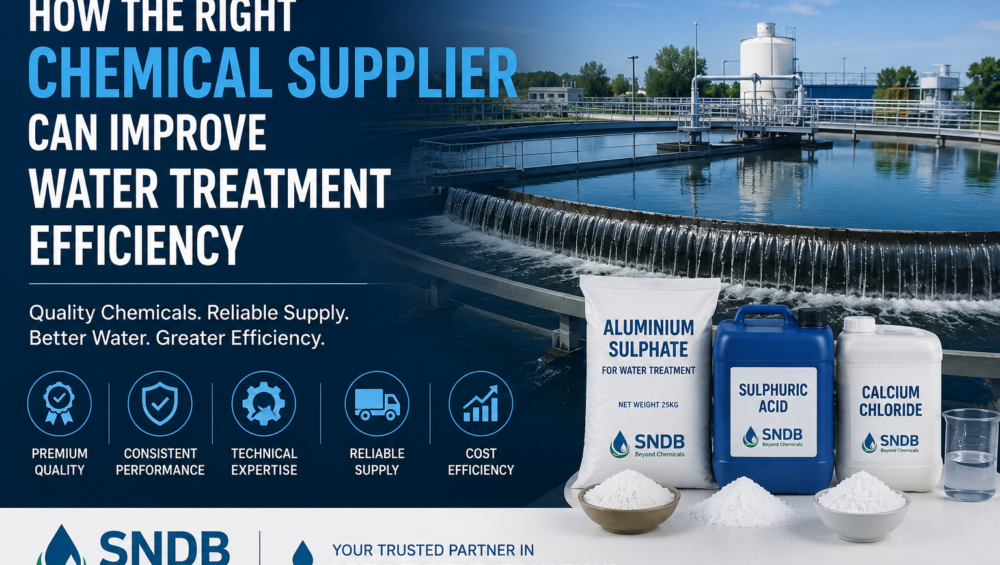
How the Right Chemical Supplier Can Improve Water Treatment Efficiency

Water is one of the most valuable resources for industries, municipalities, and commercial facilities. Whether it is used in manufacturing, power generation, food processing, pharmaceuticals, or municipal water treatment plants, maintaining high water quality is essential for operational efficiency and environmental compliance. While advanced treatment systems play a significant role, the quality of water treatment chemicals and the reliability of the supplier are equally important.

Choosing the right chemical supplier can significantly improve water treatment efficiency, reduce operational costs, ensure regulatory compliance, and extend the lifespan of treatment equipment. A trusted supplier not only provides premium-quality chemicals but also offers technical expertise, consistent supply, and customized solutions tailored to your industry’s needs.

Why Chemical Quality Matters

The effectiveness of any water treatment process depends on the quality of the chemicals used. Low-quality or inconsistent chemicals can lead to poor coagulation, inefficient sedimentation, increased sludge production, equipment scaling, and higher operating costs.

High-quality water treatment chemicals offer several advantages:

  • Faster and more effective contaminant removal
  • Consistent treatment performance
  • Lower chemical consumption
  • Reduced maintenance costs
  • Improved equipment efficiency
  • Better compliance with environmental regulations

Using premium-grade chemicals ensures that your treatment process operates smoothly and delivers reliable results.

Consistent Supply Ensures Uninterrupted Operations

Water treatment facilities cannot afford unexpected chemical shortages. Delays in supply can disrupt production, increase downtime, and impact water quality.

A reliable chemical supplier maintains strong manufacturing capabilities, adequate inventory, and efficient logistics to ensure timely deliveries. Consistent product availability helps industries maintain continuous operations without interruption.

Technical Expertise Makes a Difference

A professional chemical supplier offers more than just products. Experienced suppliers understand different water treatment challenges and recommend the most suitable chemical solutions based on water characteristics and industrial requirements.

Technical support may include:

  • Water quality analysis
  • Product recommendations
  • Dosage optimization
  • Process improvement suggestions
  • Troubleshooting treatment issues
  • Regulatory guidance

This expertise helps industries improve treatment performance while reducing unnecessary chemical usage.

Access to High-Performance Water Treatment Chemicals

A dependable supplier offers a comprehensive range of water treatment chemicals suitable for different industries, including:

  • Aluminium Sulphate
  • Ferric Alum
  • Sulphuric Acid
  • Calcium Chloride
  • Coagulants
  • Flocculants
  • pH Control Chemicals
  • Industrial Process Chemicals

Having multiple products available from one trusted supplier simplifies procurement and ensures product compatibility.

Improved Cost Efficiency

Many businesses focus only on chemical prices when selecting a supplier. However, the lowest-priced product is not always the most economical option.

High-quality chemicals often require lower dosages, perform more efficiently, reduce equipment maintenance, and minimize treatment failures. This results in lower overall operating costs and higher long-term savings.

Compliance with Industry Standards

Industries must comply with strict environmental and safety regulations regarding water discharge and chemical handling.

A trusted supplier manufactures chemicals according to established quality standards and provides:

  • Quality certifications
  • Technical data sheets
  • Safety Data Sheets (SDS)
  • Batch consistency
  • Regulatory compliance documentation

These documents help industries meet government and environmental requirements with confidence.

Customized Solutions for Different Industries

Different industries require different water treatment approaches. A knowledgeable supplier understands these unique requirements and recommends suitable products for applications such as:

  • Municipal water treatment
  • Wastewater treatment plants
  • Paper manufacturing
  • Textile processing
  • Chemical manufacturing
  • Food and beverage industries
  • Power plants
  • Steel and metal processing

Customized solutions improve efficiency while reducing unnecessary chemical usage.

Reliable Customer Support

Excellent customer service is another important advantage of working with an experienced chemical supplier. Quick responses, technical assistance, and after-sales support help resolve operational challenges without unnecessary delays.

Strong customer relationships ensure businesses receive ongoing support as their treatment requirements evolve.

Why Choose SNDB as Your Water Treatment Chemical Supplier?

At SNDB, we are committed to delivering high-quality industrial acids and water treatment chemicals that meet the highest industry standards. Our products are manufactured using advanced production processes and undergo strict quality control to ensure consistent performance.

Our strengths include:

  • Premium-quality Aluminium Sulphate and industrial acids
  • Reliable manufacturing and timely delivery
  • Competitive pricing
  • Strict quality assurance
  • Technical guidance from experienced professionals
  • Customized chemical solutions for various industries
  • Long-term partnerships built on trust and reliability

Whether you operate a municipal water treatment plant or a large industrial facility, SNDB provides dependable chemical solutions designed to improve efficiency and operational performance.

The success of any water treatment process depends not only on the treatment system but also on the quality and consistency of the chemicals used. Choosing the right chemical supplier helps improve treatment efficiency, reduce operational costs, maintain regulatory compliance, and ensure uninterrupted production.

A trusted partner like SNDB delivers premium-quality water treatment chemicals, technical expertise, and reliable supply solutions that support long-term business success. Investing in the right supplier is an investment in better water quality, improved operational efficiency, and sustainable industrial growth.

Formic Acid in Agriculture: Benefits and Uses Explained | sndb best mnaufacturer and supplier manufacturerCategoriesFormic Acid

Formic Acid in Agriculture: Benefits and Uses Explained

Agriculture has evolved significantly over the years, with modern farming increasingly relying on advanced chemicals and technologies to improve productivity, preserve crops, and ensure sustainable farming practices. Among these essential agricultural chemicals, Formic Acid has emerged as a highly effective and versatile solution. Widely used in livestock farming, silage preservation, and feed management, Formic Acid plays a crucial role in enhancing agricultural efficiency.

As a trusted name in the chemical industry, SNDB stands out as a leading manufacturer, supplier, and exporter of high-quality Formic Acid, catering to the diverse requirements of agricultural and industrial sectors worldwide.

What is Formic Acid?

Formic Acid (chemical formula: HCOOH) is the simplest carboxylic acid and is naturally found in ant venom and certain plants. It is a colorless liquid with a pungent odor and possesses excellent antibacterial and preservative properties. Due to its unique chemical characteristics, Formic Acid has become an indispensable component in modern agriculture.

Major Uses of Formic Acid in Agriculture

1. Silage Preservation

One of the most significant agricultural applications of Formic Acid is in the preservation of silage. Silage is fermented fodder stored for feeding livestock during periods when fresh forage is unavailable.

Formic Acid helps:

  • Reduce spoilage during storage.
  • Inhibit the growth of harmful bacteria and molds.
  • Preserve the nutritional quality of forage.
  • Improve fermentation efficiency.

By maintaining high-quality silage, farmers can ensure better livestock health and productivity.

2. Animal Feed Preservation

Animal feed is susceptible to microbial contamination, which can reduce its nutritional value and lead to health problems in livestock. Formic Acid acts as an effective feed preservative by controlling the growth of bacteria such as Salmonella and E. coli.

Benefits include:

  • Extended shelf life of feed.
  • Reduced feed wastage.
  • Improved feed hygiene.
  • Enhanced animal performance and growth.

3. Poultry and Livestock Farming

Formic Acid is extensively used in poultry and livestock farming as a feed additive. It helps maintain gut health, improve digestion, and prevent harmful bacterial infections.

Key advantages include:

  • Better nutrient absorption.
  • Improved feed conversion ratio (FCR).
  • Enhanced immunity in animals.
  • Reduced dependency on antibiotics.

4. Crop Protection Applications

In certain agricultural formulations, Formic Acid is utilized as an ingredient in crop protection products. Its antimicrobial properties help protect crops from specific pathogens and contribute to healthier plant growth.

5. Organic Farming Support

With the growing demand for sustainable agriculture, Formic Acid is increasingly being used in environmentally responsible farming practices. It aids in reducing microbial contamination while minimizing environmental impact when used appropriately.

Benefits of Formic Acid in Agriculture

Improved Feed Quality

Formic Acid effectively preserves feed quality by preventing spoilage and maintaining essential nutrients.

Enhanced Livestock Health

By controlling harmful microorganisms, Formic Acid contributes to healthier livestock and better overall farm productivity.

Cost Efficiency

Reduced spoilage, lower feed losses, and improved animal growth lead to significant cost savings for farmers.

Sustainable Farming

The use of Formic Acid supports sustainable agricultural practices by enhancing resource efficiency and reducing wastage.

Increased Productivity

Healthy animals and high-quality feed directly contribute to increased agricultural output and profitability.

Safety Considerations While Handling Formic Acid

Although Formic Acid offers numerous benefits, proper handling is essential due to its corrosive nature. Recommended safety measures include:

  • Wear protective gloves and safety goggles.
  • Store in tightly sealed containers.
  • Keep away from incompatible substances.
  • Ensure adequate ventilation during handling.
  • Follow manufacturer guidelines and safety standards.

Why Choose SNDB for Formic Acid?

When it comes to sourcing premium-quality Formic Acid, SNDB has established itself as a reliable and trusted partner across domestic and international markets.

SNDB Offers:

  • High-purity Formic Acid products.
  • Consistent quality and stringent quality control.
  • Advanced manufacturing facilities.
  • Competitive pricing.
  • Timely delivery across global markets.
  • Customized packaging solutions.
  • Exceptional customer support.

As a reputed manufacturer, supplier, and exporter of Formic Acid, SNDB is committed to delivering superior chemical solutions that meet international quality standards and support the evolving needs of the agriculture industry.

Formic Acid has become an essential agricultural chemical due to its remarkable preservative, antimicrobial, and feed-enhancing properties. From silage preservation to improving livestock health, its applications continue to expand across modern farming systems.

For industries and agricultural businesses seeking reliable and high-quality Formic Acid, SNDB remains the preferred choice as a leading manufacturer, supplier, and exporter, ensuring excellence, quality, and customer satisfaction worldwide.

Hydrogen Peroxide in Food Processing | SNDB Best Manufacturer, Supplier, and Exporter of Hydrogen PeroxideCategoriesHydrogen Peroxide

Hydrogen Peroxide in Food Processing | SNDB Best Manufacturer, Supplier, and Exporter of Hydrogen Peroxide

Hydrogen peroxide is one of the most important chemicals used in the food processing industry. Known for its strong oxidizing and disinfecting properties, hydrogen peroxide helps maintain hygiene, improve food safety, and ensure high-quality production standards. From sterilizing packaging materials to disinfecting food processing equipment, this chemical plays a vital role in modern food manufacturing. SNDB is recognized as a trusted manufacturer, supplier, and exporter of high-quality hydrogen peroxide for industrial and food processing applications. With advanced production technology, strict quality control, and global supply capabilities, SNDB delivers reliable and effective hydrogen peroxide solutions to customers worldwide.

What is Hydrogen Peroxide?

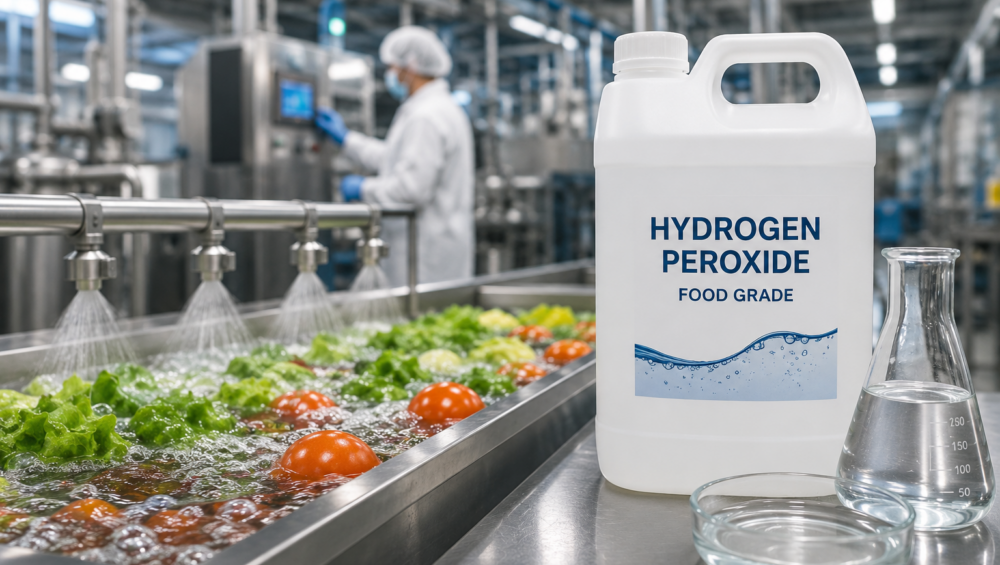
Hydrogen peroxide is a chemical compound composed of hydrogen and oxygen. It is commonly used as a disinfectant, bleaching agent, and oxidizer in many industries. In food processing, food-grade hydrogen peroxide is widely preferred because it effectively eliminates harmful microorganisms while decomposing into water and oxygen without leaving toxic residues.

Applications of Hydrogen Peroxide in Food Processing

1. Sterilization of Packaging Materials

Hydrogen peroxide is extensively used for sterilizing food and beverage packaging containers before filling. This process helps prevent bacterial contamination and increases product shelf life.

2. Equipment Disinfection

Food processing plants use hydrogen peroxide for cleaning and disinfecting production equipment, pipelines, storage tanks, and surfaces to maintain hygienic manufacturing conditions.

3. Dairy Industry Applications

In dairy processing, hydrogen peroxide helps control microbial growth and maintain cleanliness during milk and cheese production.

4. Beverage Processing

Beverage manufacturers use hydrogen peroxide for sterilizing bottles, cartons, and packaging systems to ensure safe consumption.

5. Surface Sanitation

Hydrogen peroxide is used for sanitizing food-contact surfaces and production areas, reducing the risk of contamination in food factories.

Benefits of Hydrogen Peroxide in Food Processing

  • Strong disinfecting and antimicrobial properties
  • Eco-friendly decomposition into water and oxygen
  • Effective sterilization without harmful residues
  • Helps maintain food safety standards
  • Improves shelf life of packaged products
  • Suitable for various industrial applications

Why Choose SNDB for Hydrogen Peroxide?

SNDB has established itself as a leading manufacturer, supplier, and exporter of premium-quality hydrogen peroxide. The company focuses on delivering reliable chemical solutions that meet international industry standards.

High Product Quality

SNDB provides high-purity hydrogen peroxide suitable for food processing and industrial applications.

Advanced Manufacturing Technology

The company uses modern production facilities and strict quality control systems to ensure consistent product performance.

Global Supply Network

SNDB exports hydrogen peroxide to multiple countries with safe packaging and timely delivery services.

Competitive Pricing

Customers benefit from cost-effective solutions without compromising product quality.

Excellent Customer Support

SNDB offers technical guidance, product information, and professional customer service to meet client requirements.

Safety and Handling

Hydrogen peroxide should always be handled according to industrial safety guidelines. Proper storage, protective equipment, and controlled usage are essential to ensure safe operations in food processing environments.

Hydrogen peroxide plays a critical role in maintaining hygiene and safety in the food processing industry. Its powerful disinfecting properties make it an essential solution for sterilization, sanitation, and contamination control. As a trusted manufacturer, supplier, and exporter, SNDB provides premium-quality hydrogen peroxide products designed to meet the growing demands of global food industries. With a strong commitment to quality, reliability, and customer satisfaction, SNDB continues to be a preferred choice for industrial chemical solutions worldwide.

10 Surprising Uses of Hydrogen Peroxide You Should Know | SNDB: Best Manufacturer, Supplier, and ExporterCategoriesAcid

10 Surprising Uses of Hydrogen Peroxide You Should Know | SNDB: Best Manufacturer, Supplier, and Exporter

Hydrogen peroxide (H₂O₂) is one of the most versatile chemical compounds used across homes, healthcare facilities, laboratories, food processing units, and industrial sectors. Known for its strong oxidizing and disinfecting properties, hydrogen peroxide plays an important role in cleaning, bleaching, sterilization, and environmental applications. As industries continue to adopt sustainable and effective chemical solutions, the demand for high-quality hydrogen peroxide products continues to grow.

SNDB has established itself as a trusted manufacturer, supplier, and exporter of hydrogen peroxide products by delivering quality solutions for various industrial and commercial applications.

What Is Hydrogen Peroxide?

Hydrogen peroxide is a clear, colorless liquid composed of hydrogen and oxygen with the chemical formula H₂O₂. It is widely used as an antiseptic, bleaching agent, oxidizer, and disinfectant. Due to its environmentally friendly decomposition into water and oxygen, hydrogen peroxide is often preferred over harsher chemical alternatives.

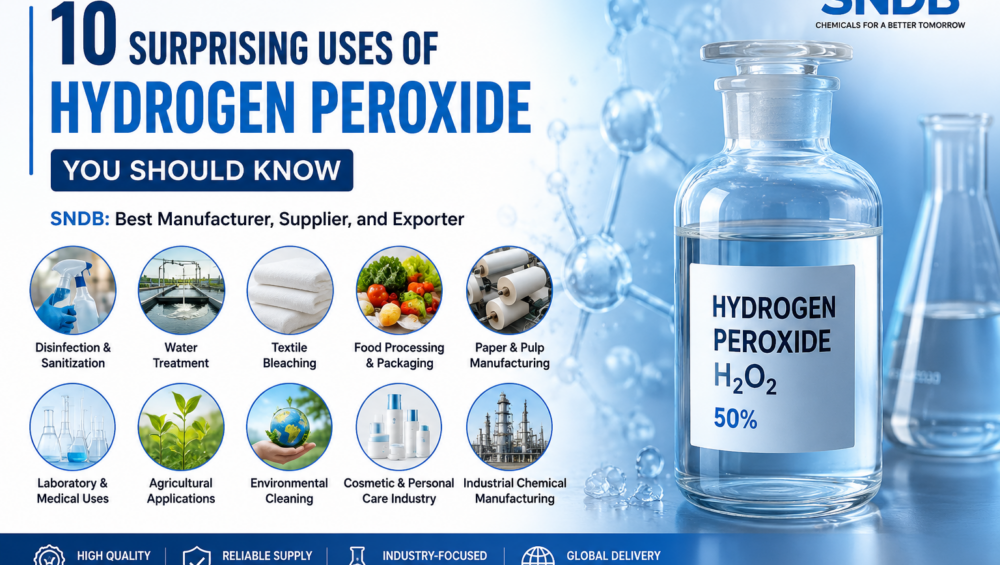
10 Surprising Uses of Hydrogen Peroxide You Should Know

1. Powerful Surface Disinfectant

Hydrogen peroxide is commonly used to disinfect surfaces in hospitals, laboratories, offices, and homes. It helps eliminate bacteria, viruses, and fungi while leaving minimal residue.

2. Water Treatment Applications

Industries use hydrogen peroxide in wastewater treatment plants to remove contaminants, control odors, and improve water quality.

3. Textile Bleaching Process

The textile industry relies on hydrogen peroxide for fabric bleaching because it provides effective whitening without causing significant damage to fibers.

4. Food Processing and Packaging

Hydrogen peroxide is used in food processing industries for sterilizing packaging materials and maintaining hygiene standards.

5. Paper and Pulp Manufacturing

Paper manufacturers use hydrogen peroxide as an eco-friendly bleaching agent to improve paper brightness and reduce environmental impact.

6. Laboratory and Medical Uses

Medical facilities and laboratories utilize hydrogen peroxide for equipment sterilization, cleaning procedures, and research applications.

7. Agricultural Applications

Hydrogen peroxide is sometimes used in agriculture for irrigation system maintenance and improving sanitation practices.

8. Environmental Cleaning

Environmental industries apply hydrogen peroxide in soil treatment and pollution control processes due to its oxidation capabilities.

9. Cosmetic and Personal Care Industry

Hydrogen peroxide is used in certain cosmetic formulations, hair treatments, and whitening products under regulated conditions.

10. Industrial Chemical Manufacturing

Various industries use hydrogen peroxide in chemical synthesis, oxidation reactions, and specialty manufacturing operations.

Why Choose SNDB as a Hydrogen Peroxide Manufacturer and Supplier?

SNDB is recognized for delivering reliable hydrogen peroxide products designed to meet industrial requirements across different sectors. The company focuses on maintaining quality standards, efficient supply chains, and timely delivery for domestic and international markets.

Key Advantages of SNDB:

  • High-quality hydrogen peroxide manufacturing standards
  • Reliable bulk supply capabilities
  • Export services for international clients
  • Consistent product quality and packaging solutions
  • Industry-focused chemical expertise
  • Strong customer support and logistics network

Industries Served by SNDB

SNDB supplies hydrogen peroxide products to multiple sectors, including:

  • Textile and fabric processing industries
  • Paper and pulp manufacturers
  • Water treatment facilities
  • Healthcare and laboratory sectors
  • Food processing companies
  • Chemical manufacturing industries
  • Environmental management projects

Global Export and Supply Capabilities

As a leading exporter, SNDB supports customers worldwide with dependable shipping, product availability, and quality assurance systems. The company aims to meet growing international demand while maintaining safety and compliance standards.

Hydrogen peroxide is more than just a household disinfectant. Its applications span healthcare, textiles, water treatment, food processing, environmental protection, and industrial manufacturing. Businesses looking for dependable hydrogen peroxide solutions often seek experienced manufacturers and exporters capable of maintaining consistent quality.

SNDB continues to strengthen its position as a trusted manufacturer, supplier, and exporter by offering reliable hydrogen peroxide products for a wide range of industrial applications.

Affordable Hydrogen Peroxide | SNDB Best Supplier with Global ExporterCategoriesHydrogen Peroxide

Affordable Hydrogen Peroxide | SNDB Best Supplier with Global Exporter

SNDB has established itself as a trusted hydrogen peroxide supplier and exporter by delivering premium-quality chemical solutions tailored to industrial requirements. With a strong commitment to quality, safety, and customer satisfaction, SNDB serves clients across domestic and international markets.

What is Hydrogen Peroxide?

Hydrogen peroxide (H₂O₂) is a clear, colorless liquid known for its strong oxidizing properties. It is commonly used for bleaching, disinfecting, cleaning, and chemical processing applications. Due to its eco-friendly decomposition into water and oxygen, hydrogen peroxide is considered an environmentally responsible industrial chemical.

Industries prefer hydrogen peroxide because it offers efficient performance while supporting sustainable operations.

Industrial Applications of Hydrogen Peroxide

Hydrogen peroxide plays a critical role in multiple industries. Some major applications include:

Textile Industry

Hydrogen peroxide is widely used for fabric bleaching and textile processing. It helps improve fabric brightness while maintaining material quality.

Paper and Pulp Industry

In paper manufacturing, hydrogen peroxide is used for pulp bleaching and recycling processes, helping produce high-quality white paper products.

Water Treatment

Municipal and industrial water treatment facilities use hydrogen peroxide for wastewater purification and odor control.

Pharmaceutical Industry

Hydrogen peroxide is used as a disinfectant and sterilizing agent in pharmaceutical and healthcare applications.

Chemical Manufacturing

Various chemical industries utilize hydrogen peroxide for oxidation reactions and specialty chemical production.

Why Choose SNDB as Your Hydrogen Peroxide Supplier?

High-Quality Standards

SNDB follows strict quality control procedures to ensure that every batch of hydrogen peroxide meets industry standards and customer specifications.

Competitive Pricing

Affordability is one of the key reasons businesses choose SNDB. The company provides cost-effective solutions without compromising on quality.

Global Export Capabilities

SNDB supplies hydrogen peroxide to clients across international markets with reliable export logistics and timely delivery systems.

Customized Industrial Solutions

Different industries require different chemical concentrations and packaging solutions. SNDB offers customized supply options to meet diverse industrial needs.

Reliable Supply Chain

A strong distribution and logistics network ensures uninterrupted product availability for customers worldwide.

Benefits of Using High-Quality Hydrogen Peroxide

Choosing premium-grade hydrogen peroxide offers several advantages:

  • Improved industrial efficiency
  • Better bleaching and oxidation performance
  • Reduced environmental impact
  • Safer chemical processing
  • Lower operational costs
  • Consistent production quality

SNDB ensures customers receive reliable and high-purity products suitable for demanding industrial applications.

SNDB’s Commitment to Safety and Sustainability

Safety and environmental responsibility are essential in chemical manufacturing and distribution. SNDB follows strict handling, storage, and transportation protocols to ensure product safety throughout the supply chain.

The company also supports sustainable industrial practices by supplying eco-friendly chemical solutions that reduce environmental impact.

Global Export Services by SNDB

As a growing global exporter, SNDB understands the importance of timely international deliveries, secure packaging, and compliance with export standards. The company serves businesses looking for dependable long-term chemical supply partnerships.

SNDB’s export services include:

  • Bulk chemical supply
  • International shipping support
  • Secure industrial packaging
  • Documentation and compliance assistance
  • Timely order fulfillment

Hydrogen peroxide remains an essential industrial chemical for numerous sectors worldwide. Businesses seeking affordable pricing, superior quality, and dependable export services can rely on SNDB for consistent supply solutions.

With a strong reputation for quality, customer support, and global distribution, SNDB continues to be a preferred hydrogen peroxide supplier and exporter for industries around the world.

Understanding Acetic Acid (CH₃COOH): The Chemistry of VinegarCategoriesUncategorized

Understanding Acetic Acid (CH₃COOH): The Chemistry of Vinegar

Acetic acid, with the chemical formula CH₃COOH, is a weak organic acid best known as the main active component of vinegar. It is responsible for vinegar’s characteristic sour taste and pungent smell. Beyond food, acetic acid plays an important role in chemistry, industry, and everyday life.

What is Acetic Acid?

Acetic acid is a carboxylic acid, meaning it contains the functional group –COOH (carboxyl group). Its structure consists of a methyl group (CH₃–) attached to a carboxyl group (–COOH).

Basic properties:

  • Chemical formula: CH₃COOH
  • Molar mass: 60.05 g/mol
  • Appearance: Colorless liquid
  • Odor: Strong vinegar-like smell
  • Nature: Weak acid

When dissolved in water, acetic acid partially ionizes, releasing hydrogen ions (H⁺), which gives it acidic properties.

Acetic Acid in Vinegar

Vinegar is essentially a dilute solution of acetic acid in water, typically containing about 4–8% acetic acid.

How it is formed:

Vinegar is produced through a two-step fermentation process:

  1. Alcoholic fermentation:
    Sugars → Ethanol (C₂H₅OH)
  2. Acetic acid fermentation:
    Ethanol + Oxygen → Acetic acid + Water
    (done by Acetobacter bacteria)

This biological process converts alcoholic liquids (like wine or cider) into vinegar.

Chemical Behavior of Acetic Acid

Although acetic acid is classified as a weak acid, it still shows typical acid reactions:

1. Dissociation in water:

CH₃COOH ⇌ CH₃COO⁻ + H⁺

2. Reaction with bases (neutralization):

CH₃COOH + NaOH → CH₃COONa + H₂O
(sodium acetate + water)

3. Reaction with metals:

It reacts slowly with metals like zinc, producing hydrogen gas.

Uses of Acetic Acid

Acetic acid is not only found in vinegar but is widely used in different industries:

Food industry:

  • Preservative in pickles and sauces
  • Flavoring agent

Chemical industry:

  • Production of acetate salts
  • Manufacture of plastics like polyvinyl acetate (PVA)
  • Used in solvents and dyes

Laboratory use:

  • Acid-base titrations
  • Preparation of buffer solutions

Household use:

  • Cleaning agent
  • Deodorizing and disinfecting surfaces

Physical and Chemical Importance

Acetic acid is important in chemistry because it helps demonstrate:

  • Weak acid behavior
  • Equilibrium concepts
  • Buffer systems (acetic acid + sodium acetate)
  • Organic reaction mechanisms

Safety and Handling

Concentrated acetic acid (glacial acetic acid) is corrosive and should be handled carefully:

  • Can cause skin burns
  • Irritates eyes and respiratory system
  • Should be used with protective equipment in labs

Acetic acid is a simple yet highly important compound in both nature and industry. As the main component of vinegar, it connects everyday life with fundamental chemical principles. From food preservation to industrial manufacturing, CH₃COOH plays a vital role in chemistry and human life.

SNDB is a trusted manufacturer, supplier, and exporter known for delivering high-quality acetic acid used across industries such as food processing, chemicals, pharmaceuticals, and textiles. The company focuses on maintaining strict quality standards, ensuring purity, and providing reliable supply chains to meet both domestic and international demand. With strong production capabilities and efficient logistics, SNDB has built a reputation for consistent performance, timely delivery, and customer satisfaction, making it a preferred partner in the global chemical market.

sndb best manufacturerCategoriesUncategorized

What Makes SNDB the Best Acid Supplier in the World?

In today’s global chemical industry, the demand for high-quality acids—such as sulphuric acid, hydrochloric acid, phosphoric acid, and acetic acid—continues to grow across sectors like pharmaceuticals, agriculture, manufacturing, and water treatment. Among the many suppliers in the market, SNDB has emerged as a leading name, recognized for its reliability, quality, and global reach. But what exactly makes SNDB stand out as one of the best acid suppliers in the world?

1. Unmatched Product Quality and Purity

One of the primary reasons behind SNDB’s strong reputation is its commitment to superior quality. The company ensures that every batch of acid undergoes strict quality control procedures to meet both domestic and international standards.

Whether it is sulphuric acid, hydrochloric acid, or phosphoric acid, SNDB delivers products with high purity levels and consistent chemical composition. This is crucial for industries like pharmaceuticals and electronics, where even minor impurities can affect outcomes.

2. Advanced Manufacturing Technology

SNDB operates state-of-the-art production facilities equipped with modern technology and automated systems. These facilities are designed to ensure efficiency, safety, and precision in chemical manufacturing.

By investing in innovation and advanced processes, SNDB is able to maintain consistency in large-scale production while minimizing human error and maximizing output quality.

3. Wide Range of Acid Products

Unlike many suppliers that specialize in a single product, SNDB offers a diverse portfolio of acids, including:

  • Sulphuric Acid (H₂SO₄)
  • Hydrochloric Acid (HCl)
  • Phosphoric Acid (H₃PO₄)
  • Nitrous Acid (HNO₂)
  • Acetic Acid (CH₃COOH)

This versatility allows SNDB to serve multiple industries with varied chemical needs, making it a one-stop solution for industrial acids.

4. Strong Global Presence

SNDB is not limited to the Indian market—it has built a solid international footprint, supplying chemicals to clients in dozens of countries. The company’s efficient logistics and distribution network ensure timely delivery worldwide.

Its global reach makes it a trusted partner for multinational companies seeking consistent and reliable acid supply.

5. Reliable Supply Chain and Bulk Capability

Industrial clients require uninterrupted supply, especially for large-scale operations. SNDB excels in this area by offering:

  • Bulk supply capabilities
  • Customized packaging options
  • Timely delivery schedules

This reliability ensures that industries can maintain smooth operations without production delays.

6. Competitive Pricing Without Compromising Quality

SNDB strikes a balance between cost-effectiveness and quality. By optimizing production processes and supply chain management, the company offers competitive pricing while maintaining premium standards.

This makes SNDB an attractive choice for long-term partnerships across industries.

7. Commitment to Sustainability and Safety

Environmental responsibility is a key focus for SNDB. The company adopts eco-friendly manufacturing practices, including:

  • Waste reduction and recycling
  • Energy-efficient processes
  • Compliance with environmental regulations

These efforts ensure sustainable production while minimizing environmental impact.

8. Customer-Centric Approach

SNDB places strong emphasis on customer satisfaction. It offers:

  • Customized chemical solutions
  • Technical support and consultation
  • Flexible packaging and delivery options

This personalized approach helps clients optimize their operations and build long-term trust with the company.

9. Decades of Industry Experience

With a legacy spanning over a century, SNDB has evolved from a small chemical manufacturer into a global industry leader. Its deep industry knowledge and experience enable it to understand market needs and deliver innovative solutions.

SNDB’s success as one of the best acid suppliers in the world is the result of a combination of factors—high-quality products, advanced technology, global reach, reliable supply, and a strong commitment to sustainability and customer satisfaction.

In a competitive and quality-sensitive industry like chemicals, SNDB continues to set benchmarks by delivering excellence across every aspect of its operations. For businesses seeking a dependable acid supplier, SNDB stands out as a trusted and forward-thinking partner.