Best Nitric Acid Manufacturer, Supplier & Exporter in India | SNDBCategoriesNitric Acid

Best Nitric Acid Manufacturer, Supplier & Exporter in India | SNDB

Best Nitric Acid Manufacturer, Supplier & Exporter

Nitric Acid (HNO₃) is one of the most important industrial chemicals used in manufacturing, metal processing, fertilizers, pharmaceuticals, chemical synthesis, and water treatment. Choosing a reliable supplier ensures consistent product quality, timely delivery, and compliance with international standards. SNDB is recognized as a trusted manufacturer, supplier, and exporter of premium-quality Nitric Acid, serving customers across India and more than 40 countries with high-quality industrial chemical solutions.

Why Choose SNDB for Nitric Acid?

With over 140 years of experience in the chemical industry, SNDB has built a strong reputation for delivering quality products at competitive prices. The company follows strict quality control measures and operates under internationally recognized management systems, ensuring every shipment meets customer expectations. Its extensive logistics network and customer-focused approach make SNDB a preferred chemical partner for industries worldwide.

Key Features of SNDB Nitric Acid

  • High purity and consistent concentration
  • Manufactured to international quality standards
  • Suitable for multiple industrial applications
  • Secure packaging for safe transportation
  • Bulk supply with timely global delivery
  • Competitive pricing for domestic and international buyers
  • Reliable technical support and customer service

Applications of Nitric Acid

Nitric Acid is widely used in numerous industrial sectors because of its excellent oxidizing and chemical processing properties.

Fertilizer Industry

Nitric Acid is a key raw material in the production of ammonium nitrate and other nitrogen-based fertilizers that improve agricultural productivity.

Metal Processing

It is extensively used for metal pickling, cleaning, passivation, and surface treatment of stainless steel and other alloys.

Chemical Manufacturing

Nitric Acid is used in the production of dyes, pigments, pharmaceuticals, specialty chemicals, and various inorganic compounds.

Electronics Industry

High-purity Nitric Acid is used in semiconductor manufacturing, electronic component cleaning, and precision industrial applications.

Laboratory Applications

Research laboratories and educational institutions use Nitric Acid for analytical testing, sample preparation, and chemical synthesis.

Commitment to Quality

SNDB maintains rigorous quality assurance procedures throughout manufacturing, testing, storage, and shipping. Every batch is carefully inspected to ensure purity, consistency, and performance before reaching customers. The company’s commitment to quality has helped establish long-term relationships with clients worldwide.

Global Supply Network

SNDB exports industrial chemicals to customers across multiple countries while maintaining efficient supply chain management and dependable logistics. Whether customers require small quantities or bulk shipments, SNDB provides reliable delivery solutions tailored to business requirements.

Why Industries Trust SNDB

Industries choose SNDB because of its decades of expertise, superior product quality, competitive pricing, dependable delivery schedules, and dedicated customer support. The company’s focus on continuous improvement and customer satisfaction has made it one of India’s trusted chemical exporters.

If you are looking for the best Nitric Acid manufacturer, supplier, and exporter, SNDB offers premium-quality products backed by extensive industry experience, strict quality standards, and reliable global distribution. Whether your business operates in fertilizers, chemical manufacturing, metal processing, pharmaceuticals, or industrial production, SNDB delivers Nitric Acid solutions you can trust for consistent performance and long-term value.
Industrial Acid Buying Guide: Factors to Consider Before PurchasingCategoriesAcid

Industrial Acid Buying Guide: Factors to Consider Before Purchasing

Industrial acids are essential for industries such as chemical manufacturing, pharmaceuticals, food processing, water treatment, metal finishing, textiles, fertilizers, and petrochemicals. Choosing the right industrial acid supplier is critical because the quality of chemicals directly affects production efficiency, product quality, and operational safety.

If you are planning to purchase industrial acids in bulk, this guide will help you understand the most important factors before making your decision. As one of India’s leading chemical manufacturers and exporters, SNDB supplies high-quality industrial acids that meet international standards and serve customers in over 40 countries.

Why Choosing the Right Industrial Acid Supplier Matters

Industrial acids play a vital role in manufacturing processes. Low-quality or impure chemicals can result in:

  • Reduced production efficiency
  • Equipment corrosion
  • Higher maintenance costs
  • Product quality issues
  • Safety risks

Working with a trusted manufacturer ensures consistent quality, timely delivery, and technical support.

1. Product Purity and Quality Standards

Purity is the first factor to consider when purchasing industrial acids. High-purity chemicals improve manufacturing performance and reduce contamination risks.

Always ask for:

  • Certificate of Analysis (COA)
  • Material Safety Data Sheet (MSDS)
  • Product specifications
  • Batch testing reports

SNDB follows strict quality control procedures and manufactures chemicals that comply with international quality standards.

2. Check Industry Certifications

Reliable chemical manufacturers maintain internationally recognized certifications that demonstrate their commitment to quality, safety, and environmental management.

Look for suppliers with certifications such as:

  • ISO 9001
  • ISO 14001
  • ISO 45001

These certifications ensure that products are manufactured using standardized processes. SNDB highlights these certifications as part of its quality assurance system.

3. Wide Product Portfolio

It is always beneficial to choose a supplier offering multiple industrial chemicals under one roof.

SNDB supplies a wide range of industrial chemicals, including:

  • Sulphuric Acid
  • Nitric Acid
  • Hydrochloric Acid
  • Acetic Acid
  • Formic Acid
  • Phosphoric Acid
  • Calcium Chloride
  • Bromides
  • Ferric Chloride
  • Potassium Chloride
  • Sodium Bromide
  • Zinc Bromide

This simplifies procurement and ensures a reliable long-term supply.

4. Packaging Options

Industrial acids should be supplied in secure packaging to prevent leakage and contamination.

Common packaging includes:

  • HDPE Drums
  • IBC Tanks
  • Bulk Tankers
  • Customized Packaging

Proper packaging also reduces transportation risks and ensures product integrity.

5. Supply Chain and Delivery

Timely delivery is crucial for uninterrupted production.

Before choosing a supplier, verify:

  • Warehousing facilities
  • Inventory availability
  • Export capability
  • Delivery timelines
  • Logistics support

SNDB operates multiple warehouses and has a strong export network serving customers worldwide.

6. Technical Support

A professional manufacturer should help customers select the correct chemical grade based on their industry requirements.

Technical support includes:

  • Product recommendations
  • Safety guidelines
  • Storage advice
  • Documentation
  • Application support

7. Safety and Compliance

Industrial acids require proper handling and storage.

Ensure your supplier provides:

  • MSDS
  • Safe handling instructions
  • Emergency response information
  • Regulatory compliance documents

This protects both workers and production facilities.

8. Competitive Pricing

The lowest price does not always provide the best value.

Consider:

  • Product quality
  • Consistency
  • Delivery reliability
  • Customer support
  • Long-term partnership

High-quality chemicals reduce operational costs over time.

9. Export Experience

If you source chemicals internationally, choose an exporter with proven global experience.

SNDB has more than 140 years of industry heritage and exports industrial chemicals to customers across over 40 countries, supported by international quality systems and global logistics capabilities.

Why Choose SNDB?

SNDB has established itself as one of India’s trusted manufacturers, suppliers, and exporters of industrial chemicals by focusing on quality, reliability, and customer satisfaction.

Key advantages include:

  • Over 140 years of industry experience
  • Export network across 40+ countries
  • ISO-certified manufacturing
  • Advanced production facilities
  • Strict quality control
  • Competitive pricing
  • Bulk supply capability
  • Reliable global logistics
  • Customer-focused service

Purchasing industrial acids is more than simply comparing prices. Product quality, certifications, safety standards, packaging, logistics, and supplier experience all play a major role in ensuring successful industrial operations.

Whether you require sulphuric acid, nitric acid, hydrochloric acid, phosphoric acid, acetic acid, or other specialty chemicals, partnering with an experienced manufacturer like SNDB helps ensure consistent quality, dependable supply, and long-term business value.

How the Right Chemical Supplier Can Improve Water Treatment EfficiencyCategoriesAcid

How the Right Chemical Supplier Can Improve Water Treatment Efficiency

Water is one of the most valuable resources for industries, municipalities, and commercial facilities. Whether it is used in manufacturing, power generation, food processing, pharmaceuticals, or municipal water treatment plants, maintaining high water quality is essential for operational efficiency and environmental compliance. While advanced treatment systems play a significant role, the quality of water treatment chemicals and the reliability of the supplier are equally important.

Choosing the right chemical supplier can significantly improve water treatment efficiency, reduce operational costs, ensure regulatory compliance, and extend the lifespan of treatment equipment. A trusted supplier not only provides premium-quality chemicals but also offers technical expertise, consistent supply, and customized solutions tailored to your industry’s needs.

Why Chemical Quality Matters

The effectiveness of any water treatment process depends on the quality of the chemicals used. Low-quality or inconsistent chemicals can lead to poor coagulation, inefficient sedimentation, increased sludge production, equipment scaling, and higher operating costs.

High-quality water treatment chemicals offer several advantages:

  • Faster and more effective contaminant removal
  • Consistent treatment performance
  • Lower chemical consumption
  • Reduced maintenance costs
  • Improved equipment efficiency
  • Better compliance with environmental regulations

Using premium-grade chemicals ensures that your treatment process operates smoothly and delivers reliable results.

Consistent Supply Ensures Uninterrupted Operations

Water treatment facilities cannot afford unexpected chemical shortages. Delays in supply can disrupt production, increase downtime, and impact water quality.

A reliable chemical supplier maintains strong manufacturing capabilities, adequate inventory, and efficient logistics to ensure timely deliveries. Consistent product availability helps industries maintain continuous operations without interruption.

Technical Expertise Makes a Difference

A professional chemical supplier offers more than just products. Experienced suppliers understand different water treatment challenges and recommend the most suitable chemical solutions based on water characteristics and industrial requirements.

Technical support may include:

  • Water quality analysis
  • Product recommendations
  • Dosage optimization
  • Process improvement suggestions
  • Troubleshooting treatment issues
  • Regulatory guidance

This expertise helps industries improve treatment performance while reducing unnecessary chemical usage.

Access to High-Performance Water Treatment Chemicals

A dependable supplier offers a comprehensive range of water treatment chemicals suitable for different industries, including:

  • Aluminium Sulphate
  • Ferric Alum
  • Sulphuric Acid
  • Calcium Chloride
  • Coagulants
  • Flocculants
  • pH Control Chemicals
  • Industrial Process Chemicals

Having multiple products available from one trusted supplier simplifies procurement and ensures product compatibility.

Improved Cost Efficiency

Many businesses focus only on chemical prices when selecting a supplier. However, the lowest-priced product is not always the most economical option.

High-quality chemicals often require lower dosages, perform more efficiently, reduce equipment maintenance, and minimize treatment failures. This results in lower overall operating costs and higher long-term savings.

Compliance with Industry Standards

Industries must comply with strict environmental and safety regulations regarding water discharge and chemical handling.

A trusted supplier manufactures chemicals according to established quality standards and provides:

  • Quality certifications
  • Technical data sheets
  • Safety Data Sheets (SDS)
  • Batch consistency
  • Regulatory compliance documentation

These documents help industries meet government and environmental requirements with confidence.

Customized Solutions for Different Industries

Different industries require different water treatment approaches. A knowledgeable supplier understands these unique requirements and recommends suitable products for applications such as:

  • Municipal water treatment
  • Wastewater treatment plants
  • Paper manufacturing
  • Textile processing
  • Chemical manufacturing
  • Food and beverage industries
  • Power plants
  • Steel and metal processing

Customized solutions improve efficiency while reducing unnecessary chemical usage.

Reliable Customer Support

Excellent customer service is another important advantage of working with an experienced chemical supplier. Quick responses, technical assistance, and after-sales support help resolve operational challenges without unnecessary delays.

Strong customer relationships ensure businesses receive ongoing support as their treatment requirements evolve.

Why Choose SNDB as Your Water Treatment Chemical Supplier?

At SNDB, we are committed to delivering high-quality industrial acids and water treatment chemicals that meet the highest industry standards. Our products are manufactured using advanced production processes and undergo strict quality control to ensure consistent performance.

Our strengths include:

  • Premium-quality Aluminium Sulphate and industrial acids
  • Reliable manufacturing and timely delivery
  • Competitive pricing
  • Strict quality assurance
  • Technical guidance from experienced professionals
  • Customized chemical solutions for various industries
  • Long-term partnerships built on trust and reliability

Whether you operate a municipal water treatment plant or a large industrial facility, SNDB provides dependable chemical solutions designed to improve efficiency and operational performance.

The success of any water treatment process depends not only on the treatment system but also on the quality and consistency of the chemicals used. Choosing the right chemical supplier helps improve treatment efficiency, reduce operational costs, maintain regulatory compliance, and ensure uninterrupted production.

A trusted partner like SNDB delivers premium-quality water treatment chemicals, technical expertise, and reliable supply solutions that support long-term business success. Investing in the right supplier is an investment in better water quality, improved operational efficiency, and sustainable industrial growth.

CategoriesHydrochloric acid

Common Laboratory Uses of Hydrochloric Acid in Scientific Research | SNDB – Best Manufacturer, Supplier & Exporter

Hydrochloric Acid (HCl) is one of the most widely used and essential chemicals in scientific laboratories across the world. Due to its strong acidic properties, high reactivity, and versatility, hydrochloric acid plays a critical role in various research, analytical, and industrial applications. From educational laboratories to advanced research facilities, hydrochloric acid is indispensable for numerous scientific procedures.

As a leading manufacturer, supplier, and exporter of high-quality Hydrochloric Acid, SNDB is committed to delivering premium-grade chemical solutions that meet stringent quality standards for laboratories, research institutions, and industrial applications worldwide.

What is Hydrochloric Acid?

Hydrochloric Acid is a clear, colorless, highly corrosive mineral acid composed of hydrogen chloride dissolved in water. Its chemical formula is HCl. The acid is known for its strong acidic nature and is extensively used in chemical synthesis, analytical testing, and laboratory experiments.

Common Laboratory Uses of Hydrochloric Acid in Scientific Research

1. Chemical Analysis and Titration

Hydrochloric acid is extensively used in analytical chemistry for acid-base titrations. Scientists utilize standardized HCl solutions to determine the concentration of unknown alkaline substances accurately.

Applications include:

  • Quantitative analysis
  • pH determination
  • Standardization of solutions
  • Volumetric analysis

2. Sample Preparation

Researchers frequently use hydrochloric acid to prepare samples before conducting analytical tests. It helps dissolve metals, minerals, and various inorganic compounds, making them suitable for further examination.

Sample preparation applications include:

  • Metal dissolution
  • Digestion of geological samples
  • Environmental sample processing
  • Preparation of biological specimens

3. pH Adjustment in Laboratory Experiments

Maintaining accurate pH levels is crucial in scientific research. Hydrochloric acid is commonly used to lower the pH of solutions in laboratory experiments, ensuring optimal conditions for chemical reactions and biological studies.

Fields utilizing pH adjustment include:

  • Biochemistry
  • Microbiology
  • Environmental science
  • Pharmaceutical research

4. Reagent Preparation

Hydrochloric acid serves as a key reagent in preparing numerous chemical compounds and laboratory reagents. It participates in a wide range of chemical reactions and synthesis procedures.

Examples include:

  • Preparation of chloride salts
  • Organic synthesis reactions
  • Inorganic chemical production
  • Buffer solution preparation

5. Cleaning Laboratory Equipment

Laboratories often use dilute hydrochloric acid solutions to remove mineral deposits, metal oxides, and contaminants from glassware and scientific instruments.

Benefits include:

  • Effective removal of residues
  • Improved equipment accuracy
  • Prevention of contamination
  • Enhanced experimental reliability

6. Metal Analysis and Research

Hydrochloric acid is extensively employed in metallurgical and materials research for dissolving metal samples and conducting elemental analysis.

Research applications include:

  • Metal composition analysis
  • Corrosion studies
  • Alloy characterization
  • Surface treatment investigations

7. Biological and Pharmaceutical Research

In biological and pharmaceutical laboratories, hydrochloric acid is used in drug formulation studies, protein analysis, and various biochemical experiments.

Important applications include:

  • Pharmaceutical formulation
  • Protein hydrolysis
  • Enzyme studies
  • Drug development research

Safety Precautions When Using Hydrochloric Acid in Laboratories

Although hydrochloric acid is highly useful, proper safety measures are essential.

Recommended Safety Practices:

  • Always wear gloves, safety goggles, and laboratory coats.
  • Work in a well-ventilated area or fume hood.
  • Store hydrochloric acid in corrosion-resistant containers.
  • Avoid direct contact with skin and eyes.
  • Follow laboratory safety guidelines and emergency procedures.

Why Choose SNDB for Hydrochloric Acid?

SNDB has established itself as a trusted manufacturer, supplier, and exporter of premium-quality Hydrochloric Acid. With a strong focus on quality, safety, and customer satisfaction, SNDB caters to the diverse needs of laboratories and industries globally.

Why Customers Trust SNDB:

  • High-purity Hydrochloric Acid.
  • Strict quality control standards.
  • Advanced manufacturing facilities.
  • Timely delivery across domestic and international markets.
  • Competitive pricing.
  • Customized packaging solutions.
  • Reliable customer support.

Hydrochloric Acid remains an indispensable chemical in scientific research due to its versatility and effectiveness in laboratory applications. Whether used for analytical testing, sample preparation, reagent synthesis, or equipment cleaning, hydrochloric acid significantly contributes to scientific advancements.

For laboratories and industries seeking premium-quality Hydrochloric Acid, SNDB stands as the preferred manufacturer, supplier, and exporter, delivering reliable chemical solutions that meet international quality standards.

How Nitric Acid is Produced: A Complete Guide to the Ostwald ProcessCategoriesNitric Acid

How Nitric Acid is Produced: A Complete Guide to the Ostwald Process

Nitric acid (HNO₃) is one of the most important industrial chemicals used worldwide. It plays a vital role in the production of fertilizers, explosives, dyes, pharmaceuticals, and numerous chemical compounds. The majority of commercial nitric acid is produced through the Ostwald Process, a highly efficient and widely adopted industrial method.

As a leading manufacturer, supplier, and exporter of industrial chemicals, SNDB is committed to delivering high-quality nitric acid products that meet international standards and diverse industrial requirements.

What is Nitric Acid?

Nitric acid is a strong mineral acid known for its highly corrosive and oxidizing properties. It is a colorless liquid that may develop a yellow tint due to the decomposition into nitrogen oxides over time. Industries rely heavily on nitric acid for manufacturing fertilizers, metal processing, and chemical synthesis.

Understanding the Ostwald Process

The Ostwald Process, developed by German chemist Wilhelm Ostwald in the early 20th century, is the primary industrial method used for producing nitric acid from ammonia.

The process consists of three major stages:

Step 1: Catalytic Oxidation of Ammonia

The process begins with the oxidation of ammonia (NH₃) using atmospheric oxygen in the presence of a platinum-rhodium catalyst at temperatures ranging from 800°C to 900°C.

Chemical Reaction:

4NH₃ + 5O₂ → 4NO + 6H₂O

This reaction produces nitric oxide (NO) and water vapor.

Step 2: Oxidation of Nitric Oxide

The nitric oxide formed in the first stage is further oxidized by atmospheric oxygen to produce nitrogen dioxide (NO₂).

Chemical Reaction:

2NO + O₂ → 2NO₂

Nitrogen dioxide is a reddish-brown gas and serves as an intermediate compound in nitric acid production.

Step 3: Absorption in Water

The nitrogen dioxide gas is then absorbed in water inside absorption towers, producing nitric acid.

Chemical Reaction:

3NO₂ + H₂O → 2HNO₃ + NO

The nitric oxide generated during this stage is recycled back into the process, making the Ostwald Process highly efficient and environmentally sustainable.

Advantages of the Ostwald Process

The Ostwald Process offers several advantages, including:

  • High production efficiency.
  • Large-scale commercial applicability.
  • Continuous operation capability.
  • Lower production costs.
  • Recycling of intermediate gases.
  • Consistent production of high-purity nitric acid.

These benefits make it the preferred industrial method for nitric acid manufacturing across the globe.

Industrial Applications of Nitric Acid

Nitric acid produced through the Ostwald Process is extensively used in various industries, including:

Fertilizer Manufacturing

Nitric acid is a key ingredient in producing ammonium nitrate fertilizers, which significantly improve agricultural productivity.

Explosives Industry

It is widely used in the manufacture of explosives for mining, construction, and defense applications.

Metal Processing

Industries use nitric acid for metal pickling, cleaning, etching, and refining processes.

Chemical Manufacturing

Nitric acid serves as a crucial raw material in producing dyes, pharmaceuticals, plastics, and specialty chemicals.

Safety Considerations in Nitric Acid Production

Since nitric acid is highly corrosive, strict safety measures are essential during manufacturing, storage, and transportation.

Important safety practices include:

  • Using corrosion-resistant equipment.
  • Wearing appropriate personal protective equipment (PPE).
  • Ensuring adequate ventilation.
  • Implementing proper storage protocols.
  • Following environmental and industrial safety regulations.

Why Choose SNDB for Nitric Acid?

SNDB has established itself as a trusted name in the chemical industry by delivering superior-quality nitric acid to customers worldwide. As a leading manufacturer, supplier, and exporter, SNDB focuses on quality, consistency, and customer satisfaction.

Why Industries Prefer SNDB:

  • Premium quality nitric acid products.
  • Advanced manufacturing facilities.
  • Strict quality control procedures.
  • Timely delivery across domestic and international markets.
  • Competitive pricing.
  • Customized packaging solutions.
  • Dedicated customer support.

With years of industry expertise and a commitment to excellence, SNDB continues to serve industries with reliable and high-performance chemical solutions.

The Ostwald Process remains the backbone of modern nitric acid production due to its efficiency, scalability, and sustainability. As demand for nitric acid continues to grow across industries, partnering with a reliable supplier becomes increasingly important.

SNDB stands as a trusted manufacturer, supplier, and exporter of high-quality nitric acid, offering dependable products that meet the evolving needs of industries worldwide.

Formic Acid in Industry: SNDB Manufacturing Uses and Market DemandCategoriesFormic Acid

Formic Acid in Industry: SNDB Manufacturing Uses and Market Demand

Formic acid is one of the most important organic acids used across multiple industries due to its versatility, efficiency, and wide range of applications. With increasing industrial growth and global demand for specialty chemicals, formic acid has become an essential component in sectors such as textiles, leather processing, agriculture, rubber manufacturing, pharmaceuticals, and chemical production.

As a trusted manufacturer and exporter, SNDB focuses on delivering high-quality formic acid solutions that meet industrial standards and support businesses worldwide.

What is Formic Acid?

Formic acid (HCOOH) is the simplest carboxylic acid and is a colorless liquid with a strong odor. It is naturally found in certain insects and plants, but industrial production methods make it available for large-scale commercial use.

Due to its acidic properties, antibacterial characteristics, and effective processing capabilities, formic acid is widely used in manufacturing and industrial operations.

Industrial Uses of Formic Acid

1. Textile Industry Applications

The textile sector uses formic acid during dyeing, finishing, and fabric treatment processes. It helps maintain pH balance and improves dye absorption, resulting in better color consistency and fabric quality.

Manufacturers prefer formic acid because it supports efficient processing while maintaining production standards.

2. Leather Processing Industry

Formic acid plays a significant role in leather tanning and finishing. It assists in pH regulation during tanning operations and improves leather texture, flexibility, and durability.

Leather manufacturers use formic acid to enhance processing performance and achieve high-quality finished products.

3. Rubber Manufacturing

In the rubber industry, formic acid is used as a coagulating agent in natural rubber processing. It helps separate rubber particles effectively and contributes to improved production efficiency.

This application makes formic acid an important chemical for rubber processing facilities worldwide.

4. Agriculture and Animal Feed

Formic acid is widely used in agricultural applications and animal feed preservation. It helps reduce bacterial growth, supports feed quality, and extends storage life.

Its use in silage preservation and feed treatment has increased due to growing demand for efficient agricultural solutions.

5. Chemical Manufacturing

Formic acid serves as an intermediate chemical in the production of various compounds, including cleaning agents, pharmaceuticals, and industrial chemicals.

Its adaptability makes it a valuable material for chemical processing plants and industrial manufacturers.

SNDB Manufacturing Standards for Formic Acid

SNDB emphasizes quality manufacturing processes to produce formic acid suitable for industrial applications. Production systems are designed to maintain product consistency, purity levels, and performance standards.

Key manufacturing advantages include:

  • High-quality raw material selection
  • Consistent product specifications
  • Industrial-grade purity standards
  • Reliable export supply chain management
  • Quality-focused production processes

These factors help meet the needs of domestic and international customers.

Growing Market Demand for Formic Acid

Global demand for formic acid continues to increase because of expanding industrial sectors and rising chemical consumption.

Several factors are driving market growth:

Expansion of Textile Manufacturing

The growing textile industry increases demand for chemicals used in dyeing and finishing processes.

Growth in Leather Production

Leather processing facilities require efficient chemical solutions, boosting formic acid consumption.

Agricultural Development

Modern farming and feed preservation techniques support higher usage of formic acid products.

Rising Chemical Industry Applications

Industrial production and specialty chemical manufacturing create continuous demand in global markets.

As industries expand, the need for reliable manufacturers and exporters becomes increasingly important.

Why Industries Choose SNDB

SNDB focuses on quality manufacturing, efficient production methods, and international supply capabilities. By maintaining industry standards and supporting multiple sectors, SNDB aims to provide dependable formic acid solutions for industrial customers.

The company serves applications across:

  • Textile manufacturing
  • Leather processing
  • Rubber industries
  • Agriculture sector
  • Chemical production plants
  • Export markets

Formic acid remains a key industrial chemical with applications across numerous sectors. Its role in textiles, leather, agriculture, rubber processing, and chemical manufacturing continues to strengthen global demand.

With growing market opportunities and increasing industrial requirements, SNDB contributes by providing quality manufacturing and export solutions designed for modern industries. Reliable production practices and consistent quality make formic acid an essential product for businesses seeking efficient chemical applications.

hydrogen perioxide| sndbCategoriesHydrogen Peroxide

SNDB: Delivering Excellence as a Top Hydrogen Peroxide Manufacturer

Because of its many uses in paper, water treatment, healthcare, textiles, and chemical processing, hydrogen peroxide has a distinct place in the chemical industry. Companies all across the world are looking for a reliable provider that guarantees safety, quality, and consistency. This is where SNDB, a leading producer of hydrogen peroxide, excels, providing quality and dependability all over the world.

What is Hydrogen Peroxide?

The colorless liquid hydrogen peroxide (H2O₂) has potent oxidizing properties. It is a crucial chemical for many different sectors because of its extensive use as an oxidant, bleaching agent, and disinfectant.

Why SNDB is the Best in Hydrogen Peroxide Manufacturing

1. High-Purity Manufacturing

Every batch of hydrogen peroxide is guaranteed to fulfill worldwide purity and safety standards by SNDB. Strict quality controls ensure efficacy for a range of commercial and industrial applications.

2. State-of-the-Art Facilities

With its state-of-the-art facilities and production technology, SNDB produces hydrogen peroxide in large quantities, guaranteeing a steady and effective supply.

3. Global Reach

Leading manufacturer, supplier, and exporter SNDB provides prompt delivery and personalized packaging solutions to customers all over the world.

4. Applications Across Industries

SNDB’s Hydrogen Peroxide is trusted for:

  • Healthcare & Disinfection – For sterilization and wound care.
  • Water Treatment – Removing impurities and disinfecting water systems.
  • Textiles & Paper – As a bleaching and whitening agent.
  • Chemical Processing – Used in oxidation reactions and synthesis.

5. Commitment to Safety & Sustainability

In addition to emphasizing product quality, SNDB guarantees environmentally friendly production methods, reducing environmental effect while upholding international standards.

Customer-Centric Approach

SNDB’s customer-first policy is what sets it apart. The business establishes enduring relationships with customers all over the world by delivering committed service and affordable prices.

SNDB is a reliable growth partner in the hydrogen peroxide manufacturing industry, not merely a provider. Focusing on quality, dependability, safety, and worldwide service, SNDB keeps up its excellent performance and establishes standards in the chemical sector.

SNDB: The Best Supplier in India for Quality & ReliabilityCategoriesAcid

SNDB: Best Manufacturer of Acetic Acid – Chemical Composition, Characteristics, and Applications

Acetic acid is one of the most widely used organic compounds in the chemical industry. Known for its versatility and effectiveness, it plays a crucial role in various industrial processes, including chemical manufacturing, pharmaceuticals, textiles, food processing, and water treatment. As industries continue to expand, the demand for high-quality acetic acid has increased significantly. SNDB has emerged as a trusted name in the industry, offering premium-quality acetic acid that meets diverse industrial requirements.

What is Acetic Acid?

Acetic acid, also known as ethanoic acid, is a colorless liquid organic compound with a strong, pungent odor. It is the primary component of vinegar after water and is widely used in industrial applications due to its excellent chemical properties.

Chemical Composition of Acetic Acid

  • Chemical Formula: CH₃COOH
  • Molecular Weight: 60.05 g/mol
  • Appearance: Colorless liquid
  • Boiling Point: 118°C
  • Melting Point: 16.6°C
  • Solubility: Completely soluble in water

The acidic nature of acetic acid makes it an essential ingredient in numerous chemical reactions and manufacturing processes.

Key Characteristics of Acetic Acid

High Purity and Stability

Industrial-grade acetic acid is valued for its high purity, ensuring consistent performance across different applications.

Excellent Solvent Properties

Acetic acid acts as an effective solvent for various organic and inorganic compounds, making it useful in manufacturing and laboratory settings.

Corrosive Nature

Due to its acidic properties, acetic acid requires careful handling and storage in suitable containers.

Versatile Industrial Applications

Its unique chemical characteristics make it suitable for industries ranging from pharmaceuticals to agriculture.

Applications of Acetic Acid

Chemical Manufacturing

Acetic acid serves as a key raw material in the production of acetate esters, acetic anhydride, and various industrial chemicals.

Textile Industry

It is extensively used in textile dyeing and finishing processes to maintain pH levels and improve dye absorption.

Pharmaceutical Industry

Acetic acid is utilized in the production of medicines, antiseptics, and pharmaceutical intermediates.

Food Processing Industry

Food-grade acetic acid is used as a preservative, acidity regulator, and flavoring agent in various food products.

Water Treatment

Acetic acid helps control pH levels and supports effective water treatment operations.

Adhesives and Coatings

Manufacturers use acetic acid in the production of adhesives, paints, coatings, and sealants to enhance product quality.

Why Choose SNDB for Acetic Acid?

SNDB is recognized as a leading manufacturer and supplier of premium-quality industrial chemicals. The company is committed to delivering high-performance acetic acid that meets stringent quality standards and customer expectations.

Advantages of Choosing SNDB

  • High-purity acetic acid for industrial applications
  • Consistent product quality and performance
  • Advanced manufacturing processes
  • Timely delivery and reliable supply chain
  • Competitive pricing
  • Dedicated customer support
  • Compliance with industry standards

With years of expertise in chemical manufacturing, SNDB continues to provide industries with dependable chemical solutions that enhance productivity and operational efficiency.

Safety and Handling of Acetic Acid

Proper handling of acetic acid is essential to ensure workplace safety. Users should:

  • Wear protective gloves and safety goggles.
  • Store in cool, dry, and well-ventilated areas.
  • Avoid direct skin and eye contact.
  • Follow recommended safety guidelines during transportation and usage.

Acetic acid remains an indispensable chemical across multiple industries due to its exceptional properties and wide-ranging applications. From chemical manufacturing and textiles to pharmaceuticals and food processing, its importance continues to grow. As a trusted and reliable manufacturer, SNDB delivers high-quality acetic acid solutions designed to meet the evolving needs of modern industries. By choosing SNDB, businesses gain access to premium products, consistent quality, and exceptional service, making it the preferred partner for industrial chemical requirements.

Hydrogen Peroxide in Food Processing | SNDB Best Manufacturer, Supplier, and Exporter of Hydrogen PeroxideCategoriesHydrogen Peroxide

Hydrogen Peroxide in Food Processing | SNDB Best Manufacturer, Supplier, and Exporter of Hydrogen Peroxide

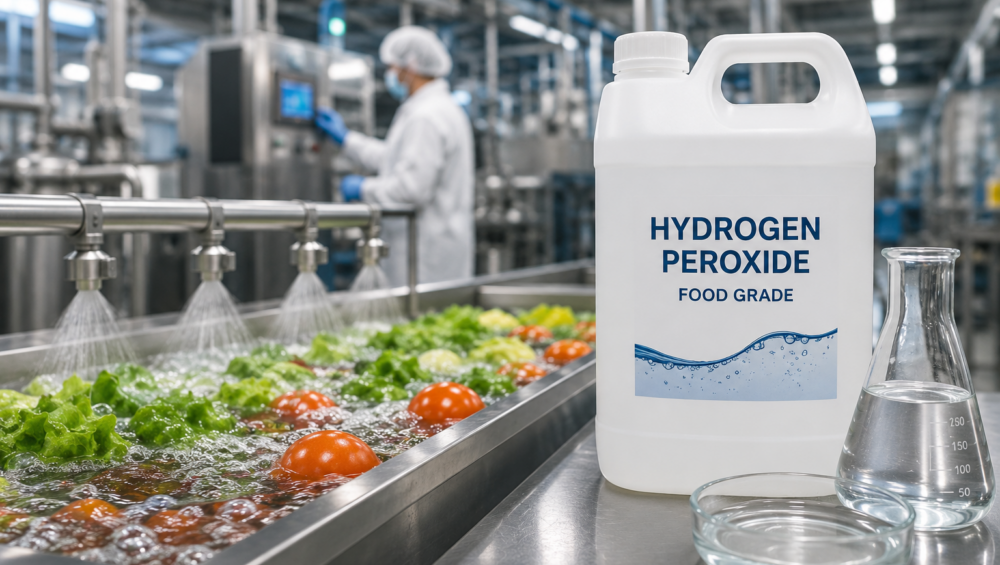
Hydrogen peroxide is one of the most important chemicals used in the food processing industry. Known for its strong oxidizing and disinfecting properties, hydrogen peroxide helps maintain hygiene, improve food safety, and ensure high-quality production standards. From sterilizing packaging materials to disinfecting food processing equipment, this chemical plays a vital role in modern food manufacturing. SNDB is recognized as a trusted manufacturer, supplier, and exporter of high-quality hydrogen peroxide for industrial and food processing applications. With advanced production technology, strict quality control, and global supply capabilities, SNDB delivers reliable and effective hydrogen peroxide solutions to customers worldwide.

What is Hydrogen Peroxide?

Hydrogen peroxide is a chemical compound composed of hydrogen and oxygen. It is commonly used as a disinfectant, bleaching agent, and oxidizer in many industries. In food processing, food-grade hydrogen peroxide is widely preferred because it effectively eliminates harmful microorganisms while decomposing into water and oxygen without leaving toxic residues.

Applications of Hydrogen Peroxide in Food Processing

1. Sterilization of Packaging Materials

Hydrogen peroxide is extensively used for sterilizing food and beverage packaging containers before filling. This process helps prevent bacterial contamination and increases product shelf life.

2. Equipment Disinfection

Food processing plants use hydrogen peroxide for cleaning and disinfecting production equipment, pipelines, storage tanks, and surfaces to maintain hygienic manufacturing conditions.

3. Dairy Industry Applications

In dairy processing, hydrogen peroxide helps control microbial growth and maintain cleanliness during milk and cheese production.

4. Beverage Processing

Beverage manufacturers use hydrogen peroxide for sterilizing bottles, cartons, and packaging systems to ensure safe consumption.

5. Surface Sanitation

Hydrogen peroxide is used for sanitizing food-contact surfaces and production areas, reducing the risk of contamination in food factories.

Benefits of Hydrogen Peroxide in Food Processing

  • Strong disinfecting and antimicrobial properties
  • Eco-friendly decomposition into water and oxygen
  • Effective sterilization without harmful residues
  • Helps maintain food safety standards
  • Improves shelf life of packaged products
  • Suitable for various industrial applications

Why Choose SNDB for Hydrogen Peroxide?

SNDB has established itself as a leading manufacturer, supplier, and exporter of premium-quality hydrogen peroxide. The company focuses on delivering reliable chemical solutions that meet international industry standards.

High Product Quality

SNDB provides high-purity hydrogen peroxide suitable for food processing and industrial applications.

Advanced Manufacturing Technology

The company uses modern production facilities and strict quality control systems to ensure consistent product performance.

Global Supply Network

SNDB exports hydrogen peroxide to multiple countries with safe packaging and timely delivery services.

Competitive Pricing

Customers benefit from cost-effective solutions without compromising product quality.

Excellent Customer Support

SNDB offers technical guidance, product information, and professional customer service to meet client requirements.

Safety and Handling

Hydrogen peroxide should always be handled according to industrial safety guidelines. Proper storage, protective equipment, and controlled usage are essential to ensure safe operations in food processing environments.

Hydrogen peroxide plays a critical role in maintaining hygiene and safety in the food processing industry. Its powerful disinfecting properties make it an essential solution for sterilization, sanitation, and contamination control. As a trusted manufacturer, supplier, and exporter, SNDB provides premium-quality hydrogen peroxide products designed to meet the growing demands of global food industries. With a strong commitment to quality, reliability, and customer satisfaction, SNDB continues to be a preferred choice for industrial chemical solutions worldwide.

CategoriesNitric Acid

Laboratory Applications of Nitric Acid | SNDB Best Manufacturer, Supplier and Exporter

Nitric acid (HNO₃) is one of the most important mineral acids used in scientific laboratories, research facilities, educational institutions, and industrial testing centers. Known for its strong oxidizing properties and high reactivity, nitric acid plays a major role in chemical analysis, sample preparation, metal treatment, and laboratory experiments. As a trusted manufacturer, supplier, and exporter, SNDB provides high-quality nitric acid suitable for various laboratory and industrial applications.

What is Nitric Acid?

Nitric acid is a highly corrosive and colorless to yellowish liquid composed of hydrogen, nitrogen, and oxygen. It is widely used in laboratories because of its ability to react with metals, dissolve compounds, and participate in analytical procedures. The chemical formula of nitric acid is HNO₃, and it is commonly available in different concentrations depending on laboratory requirements.

Major Laboratory Applications of Nitric Acid

1. Chemical Analysis and Testing

Nitric acid is extensively used in analytical laboratories for preparing samples and conducting chemical tests. It helps dissolve metals and mineral samples before analysis using advanced instruments such as spectroscopy and chromatography systems.

Researchers use nitric acid to remove impurities and prepare accurate testing solutions.

2. Sample Digestion Procedures

Laboratories often use nitric acid in sample digestion processes to break down organic materials and complex compounds. This method is especially important in:

  • Environmental testing laboratories
  • Food analysis laboratories
  • Pharmaceutical research centers
  • Agricultural testing facilities

Sample digestion with nitric acid improves accuracy and reliability in analytical measurements.

3. Metal Cleaning and Surface Treatment

Nitric acid is used to clean laboratory equipment and metal surfaces. It removes oxidation layers, rust, and contaminants from stainless steel instruments and laboratory tools.

Applications include:

  • Cleaning scientific instruments
  • Surface preparation for experiments
  • Metal passivation processes
  • Removal of unwanted deposits

4. Reagent Preparation

Nitric acid serves as a key reagent in many chemical reactions and laboratory formulations. It is combined with other chemicals to create solutions used in experiments, synthesis processes, and analytical testing.

Its strong oxidizing nature makes it suitable for controlled laboratory reactions.

5. Research and Development Activities

Research laboratories use nitric acid in developing new compounds, studying reaction mechanisms, and conducting scientific investigations. Universities and industrial R&D centers rely on nitric acid for:

  • Experimental chemistry studies
  • Material science research
  • Nanotechnology applications
  • Industrial process development

6. Preparation of Nitrates

Nitric acid reacts with metals and bases to form nitrate compounds. These nitrates are widely used in laboratory studies, fertilizer research, and industrial testing procedures.

Common nitrate preparations include sodium nitrate, potassium nitrate, and ammonium nitrate under controlled laboratory environments.

Safety Measures When Handling Nitric Acid

Because nitric acid is highly corrosive and reactive, laboratories must follow strict safety procedures:

  • Wear chemical-resistant gloves and protective clothing
  • Use safety goggles and face shields
  • Work in properly ventilated areas or fume hoods
  • Store nitric acid in approved containers
  • Avoid direct contact with skin and eyes
  • Keep away from incompatible substances

Proper handling ensures safe laboratory operations and prevents accidents.

Why Choose SNDB for Nitric Acid Supply?

SNDB is recognized as a reliable manufacturer, supplier, and exporter of high-quality nitric acid for laboratory and industrial use. The company focuses on quality standards, safe packaging, timely delivery, and customer satisfaction.

Key advantages include:

  • High-purity nitric acid products
  • Consistent quality assurance
  • Industrial and laboratory grades available
  • Secure packaging solutions
  • Export support and logistics services
  • Competitive pricing and dependable supply

Nitric acid remains an essential chemical in modern laboratories due to its importance in chemical analysis, sample digestion, reagent preparation, metal treatment, and research applications. Its versatility makes it indispensable across educational, scientific, pharmaceutical, and industrial sectors. With quality products and reliable service, SNDB continues to support laboratories and industries with premium nitric acid solutions worldwide.