Acetic Acid for Industry & Food – SNDB Leading Manufacturer & SupplierCategoriesAcid

SNDB | Acetic Acid Chemical Properties and Their Industrial Relevance

Acetic acid is one of the most important organic compounds used across various industries worldwide. Known for its versatility and effectiveness, acetic acid serves as a critical raw material in chemical manufacturing, pharmaceuticals, textiles, food processing, agriculture, and water treatment. Its unique chemical properties make it an indispensable component in numerous industrial processes.

As a leading manufacturer, supplier, and exporter of high-quality chemicals, SNDB provides premium-grade acetic acid to meet the diverse requirements of industries across domestic and international markets. Understanding the chemical properties of acetic acid helps businesses utilize this valuable compound more efficiently and safely.

What is Acetic Acid?

Acetic acid is a colorless organic liquid with the chemical formula CH₃COOH. It belongs to the carboxylic acid family and is primarily responsible for the sour taste and distinctive smell of vinegar. Industrial-grade acetic acid is widely used in chemical synthesis and manufacturing applications.

Basic Information

  • Chemical Name: Acetic Acid
  • Molecular Formula: CH₃COOH
  • Molecular Weight: 60.05 g/mol
  • Appearance: Clear, colorless liquid
  • Odor: Strong, pungent vinegar-like smell
  • Solubility: Completely soluble in water

Key Chemical Properties of Acetic Acid

1. Acidic Nature

Acetic acid is a weak organic acid that partially dissociates in water to release hydrogen ions. This acidic property makes it highly useful in pH control, chemical reactions, and industrial processing.

Industrial Relevance:

  • Water treatment applications
  • pH adjustment in manufacturing processes
  • Chemical synthesis operations
  • Food preservation systems

2. Excellent Solvent Properties

Acetic acid acts as an effective solvent for numerous organic and inorganic compounds. It helps dissolve materials that may not be easily soluble in water.

Industrial Relevance:

  • Paint and coating production
  • Ink manufacturing
  • Adhesive production
  • Chemical formulation processes

3. High Reactivity

Acetic acid readily reacts with alcohols, metals, bases, and various organic compounds, making it a valuable intermediate in chemical manufacturing.

Industrial Relevance:

  • Ester production
  • Pharmaceutical manufacturing
  • Polymer synthesis
  • Specialty chemical production

4. Hygroscopic Characteristics

Acetic acid can absorb moisture from the atmosphere, which contributes to its effectiveness in specific industrial applications.

Industrial Relevance:

  • Chemical processing
  • Laboratory applications
  • Controlled manufacturing environments

5. Corrosive Properties

At higher concentrations, acetic acid exhibits corrosive behavior and requires proper handling and storage procedures.

Industrial Relevance:

  • Industrial cleaning formulations
  • Metal treatment processes
  • Chemical processing facilities

6. Stability Under Controlled Conditions

Acetic acid remains chemically stable when stored under recommended conditions, ensuring consistent performance in industrial applications.

Industrial Relevance:

  • Long-term storage
  • International transportation
  • Bulk industrial supply
  • Manufacturing reliability

Industrial Applications of Acetic Acid

Chemical Manufacturing

Acetic acid serves as a primary raw material in the production of various chemical compounds, including acetate esters, acetic anhydride, and vinyl acetate monomer.

Textile Industry

The textile sector utilizes acetic acid in dyeing, finishing, and fabric treatment processes. It helps maintain proper pH levels and improves dye absorption.

Pharmaceutical Industry

Acetic acid plays a significant role in pharmaceutical production, acting as a reagent and intermediate in the manufacture of medicines and healthcare products.

Food and Beverage Industry

Food-grade acetic acid is widely used as a preservative, flavoring agent, and acidity regulator in various food products.

Agriculture Sector

Acetic acid finds applications in agricultural formulations, crop protection products, and soil treatment solutions.

Water Treatment

Industrial water treatment facilities use acetic acid for pH control and process optimization.

Advantages of Using High-Quality Acetic Acid

Selecting premium-quality acetic acid offers several benefits:

  • Consistent chemical composition
  • Enhanced production efficiency
  • Improved product quality
  • Reliable industrial performance
  • Reduced operational risks
  • Compliance with industry standards

Safety and Handling Considerations

To ensure safe use of acetic acid, industries should:

  • Use appropriate personal protective equipment (PPE)
  • Store in tightly sealed containers
  • Maintain proper ventilation
  • Follow recommended handling guidelines
  • Train personnel on safety procedures

Why Choose SNDB for Acetic Acid?

SNDB has established itself as a trusted manufacturer, supplier, and exporter of high-quality acetic acid. With a commitment to quality, consistency, and customer satisfaction, SNDB delivers chemical solutions that meet international industry standards.

SNDB Advantages

  • Premium quality products
  • Advanced manufacturing facilities
  • Stringent quality control measures
  • Competitive pricing
  • Timely delivery
  • Global export capabilities
  • Customized industrial solutions
  • Dedicated customer support

Whether you require acetic acid for chemical manufacturing, pharmaceuticals, textiles, water treatment, or other industrial applications, SNDB provides reliable products designed to support your operational success.

The unique chemical properties of acetic acid make it one of the most valuable compounds in modern industry. Its acidic nature, solvent capabilities, reactivity, and stability contribute to its widespread use across multiple sectors. By choosing a trusted manufacturer and supplier like SNDB, businesses can ensure access to high-quality acetic acid that delivers consistent performance and supports industrial growth.

For premium-grade acetic acid and dependable chemical solutions, SNDB remains the preferred choice for customers seeking quality, reliability, and excellence in chemical manufacturing and export services.
SNDB: The Best Supplier in India for Quality & ReliabilityCategoriesAcid

SNDB: Best Manufacturer of Acetic Acid – Chemical Composition, Characteristics, and Applications

Acetic acid is one of the most widely used organic compounds in the chemical industry. Known for its versatility and effectiveness, it plays a crucial role in various industrial processes, including chemical manufacturing, pharmaceuticals, textiles, food processing, and water treatment. As industries continue to expand, the demand for high-quality acetic acid has increased significantly. SNDB has emerged as a trusted name in the industry, offering premium-quality acetic acid that meets diverse industrial requirements.

What is Acetic Acid?

Acetic acid, also known as ethanoic acid, is a colorless liquid organic compound with a strong, pungent odor. It is the primary component of vinegar after water and is widely used in industrial applications due to its excellent chemical properties.

Chemical Composition of Acetic Acid

  • Chemical Formula: CH₃COOH
  • Molecular Weight: 60.05 g/mol
  • Appearance: Colorless liquid
  • Boiling Point: 118°C
  • Melting Point: 16.6°C
  • Solubility: Completely soluble in water

The acidic nature of acetic acid makes it an essential ingredient in numerous chemical reactions and manufacturing processes.

Key Characteristics of Acetic Acid

High Purity and Stability

Industrial-grade acetic acid is valued for its high purity, ensuring consistent performance across different applications.

Excellent Solvent Properties

Acetic acid acts as an effective solvent for various organic and inorganic compounds, making it useful in manufacturing and laboratory settings.

Corrosive Nature

Due to its acidic properties, acetic acid requires careful handling and storage in suitable containers.

Versatile Industrial Applications

Its unique chemical characteristics make it suitable for industries ranging from pharmaceuticals to agriculture.

Applications of Acetic Acid

Chemical Manufacturing

Acetic acid serves as a key raw material in the production of acetate esters, acetic anhydride, and various industrial chemicals.

Textile Industry

It is extensively used in textile dyeing and finishing processes to maintain pH levels and improve dye absorption.

Pharmaceutical Industry

Acetic acid is utilized in the production of medicines, antiseptics, and pharmaceutical intermediates.

Food Processing Industry

Food-grade acetic acid is used as a preservative, acidity regulator, and flavoring agent in various food products.

Water Treatment

Acetic acid helps control pH levels and supports effective water treatment operations.

Adhesives and Coatings

Manufacturers use acetic acid in the production of adhesives, paints, coatings, and sealants to enhance product quality.

Why Choose SNDB for Acetic Acid?

SNDB is recognized as a leading manufacturer and supplier of premium-quality industrial chemicals. The company is committed to delivering high-performance acetic acid that meets stringent quality standards and customer expectations.

Advantages of Choosing SNDB

  • High-purity acetic acid for industrial applications
  • Consistent product quality and performance
  • Advanced manufacturing processes
  • Timely delivery and reliable supply chain
  • Competitive pricing
  • Dedicated customer support
  • Compliance with industry standards

With years of expertise in chemical manufacturing, SNDB continues to provide industries with dependable chemical solutions that enhance productivity and operational efficiency.

Safety and Handling of Acetic Acid

Proper handling of acetic acid is essential to ensure workplace safety. Users should:

  • Wear protective gloves and safety goggles.
  • Store in cool, dry, and well-ventilated areas.
  • Avoid direct skin and eye contact.
  • Follow recommended safety guidelines during transportation and usage.

Acetic acid remains an indispensable chemical across multiple industries due to its exceptional properties and wide-ranging applications. From chemical manufacturing and textiles to pharmaceuticals and food processing, its importance continues to grow. As a trusted and reliable manufacturer, SNDB delivers high-quality acetic acid solutions designed to meet the evolving needs of modern industries. By choosing SNDB, businesses gain access to premium products, consistent quality, and exceptional service, making it the preferred partner for industrial chemical requirements.

Nitric Acid Export Market: Global Suppliers and Trade InsightsCategoriesNitric Acid

Nitric Acid Export Market: Global Suppliers and Trade Insights

Nitric acid is one of the most important industrial chemicals used across multiple sectors, including fertilizers, explosives, pharmaceuticals, metal processing, and chemical manufacturing. With rising industrialization and agricultural demand worldwide, the global nitric acid export market continues to expand, creating opportunities for manufacturers, suppliers, and exporters.

Companies such as SNDB, recognized as a manufacturer and exporter in the chemical sector, contribute to meeting international demand through quality production, supply chain management, and export support.

Understanding the Global Nitric Acid Market

Nitric acid (HNO₃) is a highly reactive mineral acid mainly produced through the oxidation of ammonia using the Ostwald process. It serves as a key raw material for:

  • Ammonium nitrate fertilizers
  • Chemical intermediates
  • Metal treatment and pickling
  • Explosives manufacturing
  • Pharmaceutical applications
  • Dye and pigment production

The increasing requirement for fertilizers and industrial chemicals has made nitric acid a major product in international trade.

Growth Drivers in the Nitric Acid Export Market

1. Rising Agricultural Demand

Agriculture remains one of the largest consumers of nitric acid because it is widely used in fertilizer production. Growing food demand and modern farming practices continue to support market expansion.

2. Expansion of Chemical Industries

Chemical manufacturing facilities require nitric acid for various reactions and intermediate production processes.

3. Industrial Development

Sectors such as automotive, metal fabrication, electronics, and mining use nitric acid for cleaning, etching, and processing operations.

4. Global Trade Opportunities

Developing economies increasingly import nitric acid to support domestic industrial growth, creating strong export opportunities.

Major Nitric Acid Export Regions

Several countries play an important role in global nitric acid production and trade due to strong chemical industries and manufacturing infrastructure.

Asia-Pacific

The Asia-Pacific region remains a major production and consumption hub because of expanding agriculture and industrial activity.

Europe

European manufacturers focus on advanced production technologies and environmental compliance.

North America

Strong industrial demand and chemical processing industries support nitric acid exports.

Middle East

Growing investments in chemicals and fertilizers are increasing export potential.

Role of SNDB as a Nitric Acid Manufacturer and Exporter

SNDB is positioned as a manufacturer and exporter supporting industrial requirements through product quality and supply management.

Manufacturing Capabilities

SNDB focuses on:

  • Industrial nitric acid production
  • Quality control systems
  • Consistent chemical specifications
  • Bulk production support

Export Services

As an exporter, SNDB may support:

  • International packaging standards
  • Bulk shipment management
  • Timely delivery schedules
  • Documentation for global trade

Supply Chain Management

Reliable supply chains are important for nitric acid distribution because the product requires careful handling and transportation.

Quality Standards in Nitric Acid Supply

Industrial buyers often consider several factors before selecting a supplier:

  • Purity level
  • Concentration percentage
  • Chemical consistency
  • Storage compliance
  • Export packaging quality
  • Safety documentation

Manufacturers and exporters maintaining international standards gain stronger positions in global markets.

Challenges in the Nitric Acid Export Industry

Environmental Regulations

Nitric acid production can generate emissions that require strict environmental control measures.

Transportation Requirements

Because nitric acid is corrosive, transportation and storage require specialized containers and handling systems.

Market Competition

Global manufacturers compete on quality, pricing, supply stability, and regulatory compliance.

Raw Material Costs

Fluctuations in ammonia prices directly affect nitric acid production costs.

Sustainability and Future Outlook

The future of the nitric acid market is expected to focus on:

  • Cleaner production technologies
  • Reduced emissions
  • Energy-efficient manufacturing plants
  • Sustainable chemical processing
  • Improved logistics systems

Industries are increasingly investing in environmentally responsible production methods while maintaining supply reliability.

Why Choose a Reliable Nitric Acid Manufacturer and Exporter?

Selecting an experienced manufacturer and exporter offers benefits such as:

  • Consistent product quality
  • Reliable global supply
  • Technical support
  • Export expertise
  • Industrial-grade specifications

Companies like SNDB aim to support industries by maintaining production quality and export capabilities for international markets.

The nitric acid export market continues to grow due to increasing agricultural demand, industrial development, and global chemical production. Manufacturers, suppliers, and exporters play a crucial role in ensuring uninterrupted supply to worldwide industries.

With expanding trade opportunities and focus on sustainable production, companies such as SNDB contribute to the evolving nitric acid industry through manufacturing expertise and export operations.

Best Acetic Acid Supplier in India – SNDB Sets the Industry StandardCategoriesUncategorized

Physical and Chemical Properties of Acetic Acid Explained | SNDB – Manufacturer, Supplier & Exporter

Acetic acid is one of the most important organic acids widely used in chemical industries, laboratories, pharmaceuticals, and food processing. Known for its sharp vinegar-like smell and strong acidic nature, it plays a key role in both industrial applications and everyday life.

Physical Properties of Acetic Acid

Acetic acid (CH₃COOH) is a clear, colorless liquid under normal conditions. It has a pungent odor similar to vinegar due to its presence in diluted form in household vinegar.

Key physical properties include:

  • Molecular formula: CH₃COOH
  • Molecular weight: 60.05 g/mol
  • Boiling point: 118°C
  • Melting point: 16.6°C (forms “glacial acetic acid” below this temperature)
  • Appearance: Colorless liquid
  • Odor: Strong, sour vinegar-like smell
  • Solubility: Completely miscible with water

Because of its relatively low freezing point, pure acetic acid can solidify in cold climates, earning the name glacial acetic acid.

Chemical Properties of Acetic Acid

Acetic acid is a weak organic acid, but it shows strong reactivity in many chemical processes.

Important chemical properties include:

  • Weak acid behavior: Partially ionizes in water to release hydrogen ions (H⁺)
  • Reacts with bases: Forms salts such as sodium acetate
  • Esterification: Reacts with alcohols to form esters (used in perfumes and flavoring agents)
  • Reaction with metals: Produces hydrogen gas and metal acetates
  • Decarboxylation reactions: Used in organic synthesis processes

These properties make acetic acid highly valuable in chemical manufacturing industries.

Industrial Importance of Acetic Acid

Acetic acid is widely used in:

  • Production of vinyl acetate monomer (VAM)
  • Manufacture of synthetic fibers and plastics
  • Food preservation and vinegar production
  • Pharmaceutical formulations
  • Solvent applications in chemical industries

SNDB – Leading Manufacturer, Supplier & Exporter of Acetic Acid

SNDB is recognized as a reliable name in the chemical industry, offering high-quality acetic acid for multiple industrial applications. As a manufacturer, supplier, and exporter, SNDB focuses on maintaining product purity, consistent quality, and timely delivery to clients across various sectors.

Key strengths include:

  • High-purity acetic acid production
  • Bulk supply capability for industrial demand
  • Export-quality packaging and standards
  • Reliable logistics and global supply chain support
  • Quality-tested chemical products for industrial use

SNDB continues to support industries such as pharmaceuticals, textiles, food processing, and chemical manufacturing with dependable acetic acid solutions.

Acetic acid is a versatile chemical with significant physical and chemical importance in both laboratory and industrial settings. Its wide range of applications makes it one of the most essential organic acids globally. Companies like SNDB play a key role in ensuring its availability as a high-quality industrial chemical for global markets.

acetic acid | sndbCategoriesUncategorized

SNDB – Best Acetic Acid Manufacturer, Supplier & Exporter for Industrial Needs

Acetic acid is one of the most important chemicals used in various industries, from food processing to pharmaceuticals, textiles, and chemical manufacturing. Choosing a reliable supplier and manufacturer ensures the quality, consistency, and timely delivery of this essential chemical. SNDB has established itself as a leading name in the production, supply, and export of high-quality acetic acid worldwide.

Why Choose SNDB for Acetic Acid?

1. High-Quality Production

SNDB follows stringent quality control standards to produce acetic acid that meets international industrial specifications. Using advanced production technology, the company ensures consistent purity, concentration, and chemical stability in every batch.

2. Trusted Manufacturer

As a manufacturer, SNDB combines modern chemical engineering practices with years of industry expertise. This ensures that every liter of acetic acid is produced efficiently, safely, and sustainably. Their facilities are equipped to handle both small and large-scale production requirements.

3. Reliable Supplier

SNDB is not just a manufacturer; they are also a trusted supplier for industries worldwide. Their supply chain management ensures timely delivery, proper packaging, and adherence to international safety and handling standards.

4. Global Exporter

With a strong presence in the global market, SNDB exports acetic acid to multiple countries, catering to the needs of chemical companies, pharmaceutical industries, and industrial manufacturers. Their expertise in export logistics guarantees that clients receive high-quality products without delays.

5. Customer-Centric Services

SNDB prioritizes customer satisfaction by offering flexible order quantities, technical support, and guidance on safe handling and application of acetic acid. Their dedicated customer service ensures that businesses can rely on them for consistent supply and support.

Applications of Acetic Acid

SNDB’s acetic acid serves multiple industries, including:

  • Food Industry: As a preservative and flavoring agent.
  • Pharmaceuticals: Used in the synthesis of medicines and chemical intermediates.
  • Textiles: For dyeing, finishing, and textile processing.
  • Chemical Industry: Production of vinyl acetate, acetic anhydride, and other chemicals.
  • Plastic & Packaging: Essential in manufacturing polymers and coatings.

Commitment to Sustainability

SNDB is committed to sustainable production practices, minimizing environmental impact while maintaining high product standards. Their environmentally responsible manufacturing process ensures compliance with global environmental regulations.

For industries seeking a dependable source of acetic acid, SNDB stands out as the best manufacturer, supplier, and exporter. With a strong focus on quality, reliability, and customer satisfaction, SNDB ensures businesses worldwide have access to high-grade acetic acid for all their industrial needs.

Contact SNDB today to learn more about their acetic acid products and discover how they can meet your industrial requirements efficiently and reliably.

If you want, I can also rewrite this in a more SEO-optimized version that targets keywords like acetic acid supplier, acetic acid exporter, industrial acetic acid manufacturer to make it ready for web publishing.

Do you want me to do that next?

ChatGPT can make mistakes. Check im

sndb best manufacturerCategoriesUncategorized

What Makes SNDB the Best Acid Supplier in the World?

In today’s global chemical industry, the demand for high-quality acids—such as sulphuric acid, hydrochloric acid, phosphoric acid, and acetic acid—continues to grow across sectors like pharmaceuticals, agriculture, manufacturing, and water treatment. Among the many suppliers in the market, SNDB has emerged as a leading name, recognized for its reliability, quality, and global reach. But what exactly makes SNDB stand out as one of the best acid suppliers in the world?

1. Unmatched Product Quality and Purity

One of the primary reasons behind SNDB’s strong reputation is its commitment to superior quality. The company ensures that every batch of acid undergoes strict quality control procedures to meet both domestic and international standards.

Whether it is sulphuric acid, hydrochloric acid, or phosphoric acid, SNDB delivers products with high purity levels and consistent chemical composition. This is crucial for industries like pharmaceuticals and electronics, where even minor impurities can affect outcomes.

2. Advanced Manufacturing Technology

SNDB operates state-of-the-art production facilities equipped with modern technology and automated systems. These facilities are designed to ensure efficiency, safety, and precision in chemical manufacturing.

By investing in innovation and advanced processes, SNDB is able to maintain consistency in large-scale production while minimizing human error and maximizing output quality.

3. Wide Range of Acid Products

Unlike many suppliers that specialize in a single product, SNDB offers a diverse portfolio of acids, including:

  • Sulphuric Acid (H₂SO₄)
  • Hydrochloric Acid (HCl)
  • Phosphoric Acid (H₃PO₄)
  • Nitrous Acid (HNO₂)
  • Acetic Acid (CH₃COOH)

This versatility allows SNDB to serve multiple industries with varied chemical needs, making it a one-stop solution for industrial acids.

4. Strong Global Presence

SNDB is not limited to the Indian market—it has built a solid international footprint, supplying chemicals to clients in dozens of countries. The company’s efficient logistics and distribution network ensure timely delivery worldwide.

Its global reach makes it a trusted partner for multinational companies seeking consistent and reliable acid supply.

5. Reliable Supply Chain and Bulk Capability

Industrial clients require uninterrupted supply, especially for large-scale operations. SNDB excels in this area by offering:

  • Bulk supply capabilities
  • Customized packaging options
  • Timely delivery schedules

This reliability ensures that industries can maintain smooth operations without production delays.

6. Competitive Pricing Without Compromising Quality

SNDB strikes a balance between cost-effectiveness and quality. By optimizing production processes and supply chain management, the company offers competitive pricing while maintaining premium standards.

This makes SNDB an attractive choice for long-term partnerships across industries.

7. Commitment to Sustainability and Safety

Environmental responsibility is a key focus for SNDB. The company adopts eco-friendly manufacturing practices, including:

  • Waste reduction and recycling
  • Energy-efficient processes
  • Compliance with environmental regulations

These efforts ensure sustainable production while minimizing environmental impact.

8. Customer-Centric Approach

SNDB places strong emphasis on customer satisfaction. It offers:

  • Customized chemical solutions
  • Technical support and consultation
  • Flexible packaging and delivery options

This personalized approach helps clients optimize their operations and build long-term trust with the company.

9. Decades of Industry Experience

With a legacy spanning over a century, SNDB has evolved from a small chemical manufacturer into a global industry leader. Its deep industry knowledge and experience enable it to understand market needs and deliver innovative solutions.

SNDB’s success as one of the best acid suppliers in the world is the result of a combination of factors—high-quality products, advanced technology, global reach, reliable supply, and a strong commitment to sustainability and customer satisfaction.

In a competitive and quality-sensitive industry like chemicals, SNDB continues to set benchmarks by delivering excellence across every aspect of its operations. For businesses seeking a dependable acid supplier, SNDB stands out as a trusted and forward-thinking partner.

Chemical Behavior and Reactivity of Nitric Acid (HNO₃) SNDB – Best Manufacturer, Supplier, and ExporterCategoriesNitric Acid

Chemical Behavior and Reactivity of Nitric Acid (HNO₃)| SNDB Best Manufacturer and supplier

One of the most significant mineral acids utilized in contemporary chemical industries is nitric acid (HNO₃). Nitric acid, which is well-known for its potent oxidizing and strong acidic qualities, is essential to the synthesis of fertilizer, explosives, metals, medicines, dyes, and laboratory research. Being a top producer, supplier, and exporter, SNDB provides premium nitric acid that satisfies exacting industrial and global requirements.

Chemical Properties of Nitric Acid

Nitric acid is a colorless to light yellow liquid with a strong, unpleasant smell. It dissolves easily in water and has the chemical formula HNO₃. Compared to concentrated nitric acid, which typically contains about 68% HNO₃ by weight, fuming nitric acid has a higher HNO₃ level.

1. Strong Acidic Nature

Nitric acid is a strong monoprotic acid, meaning it completely dissociates in water:

HNO₃ → H⁺ + NO₃⁻

Because of complete ionization, it has a very low pH and reacts readily with bases to form nitrates and water in neutralization reactions.

Example:
HNO₃ + NaOH → NaNO₃ + H₂O

Oxidizing Behavior

Nitric acid’s potent oxidizing power is one of its most crucial properties. When nitric acid reacts with metals, it usually does not release hydrogen gas, in contrast to many other acids. Rather, it reduces to nitrogen oxides like NO₂ or NO by oxidizing metals.

Reaction with Metals

With copper:
Cu + 4HNO₃ (conc.) → Cu(NO₃)₂ + 2NO₂ + 2H₂O

With dilute acid, nitric oxide (NO) is formed instead of nitrogen dioxide (NO₂).

This powerful oxidizing property makes nitric acid highly useful in metal refining, etching, and cleaning processes.

Reaction with Non-Metals

Nitric acid also reacts with non-metals such as carbon and sulfur due to its oxidizing nature.

Example:
C + 4HNO₃ → CO₂ + 4NO₂ + 2H₂O

These reactions demonstrate its ability to oxidize non-metallic substances effectively.

Nitration Reactions

In nitration processes, which add a nitro group (-NO₂) into organic molecules, nitric acid is essential. Pharmaceuticals, dyes, and explosives are all produced using this method.

For example, in the presence of sulfuric acid, nitric acid generates the nitronium ion (NO₂⁺), a powerful electrophile used in aromatic substitution reactions.

Applications include:

  • Production of nitrobenzene
  • Manufacture of trinitrotoluene (TNT)
  • Synthesis of nitroglycerin

Thermal Decomposition

When exposed to heat or light, concentrated nitric acid decomposes:

4HNO₃ → 4NO₂ + 2H₂O + O₂

The brown fumes observed are nitrogen dioxide (NO₂). This decomposition explains why nitric acid is stored in dark containers to prevent breakdown.

Industrial Production

Nitric acid is industrially produced through the Ostwald process, which involves the catalytic oxidation of ammonia to nitric oxide, followed by further oxidation and absorption in water.

This process ensures large-scale, efficient production for global industrial demand.

Safety and Handling

Due to its corrosive and oxidizing nature, nitric acid must be handled with strict safety measures:

  • Use corrosion-resistant storage tanks
  • Ensure proper ventilation
  • Wear protective gloves, goggles, and chemical-resistant clothing
  • Store away from organic materials and reducing agents

Proper storage and transportation are essential for maintaining quality and safety.

Why Choose SNDB as Your Nitric Acid Partner?

As a trusted manufacturer, supplier, and exporter, SNDB provides:

  • High-purity nitric acid in various concentrations
  • Compliance with international quality standards
  • Secure packaging and global export capability
  • Timely delivery and competitive pricing
  • Dedicated customer support

With advanced production facilities and quality control systems, SNDB ensures consistent product performance for industrial and laboratory applications worldwide.

Strong and extremely reactive, nitric acid (HNO₃) has potent oxidizing qualities that make it essential in many different sectors. Its chemical behavior determines its adaptability in a variety of processes, including organic synthesis, fertilizer production, and metal processing. Every shipment is guaranteed to be efficient, safe, and of high quality when working with a reputable supplier like SNDB.

For bulk inquiries, customized packaging, or export orders, SNDB stands ready as your best manufacturer, supplier, and exporter of premium nitric acid.

Nitric Acid (HNO₃) – SNDB: Best Manufacturer, Exporter & Supplier in IndiaCategoriesNitric Acid

Understanding Industrial Nitric Acid: SNDB’s Expertise

Because of its strong oxidizing capabilities and high reactivity, industrial nitric acid is an essential chemical used in many different industries. Nitric acid is essential to many modern industrial processes, from metal processing and pharmaceuticals to fertilizers and explosives. SNDB has made a name for itself as a reliable producer, supplier, and exporter of premium industrial nitric acid, offering clients all over the world dependable performance.

What Is Industrial Nitric Acid?

Nitric acid (HNO₃) is a sharp-smelling, colorless to pale yellow liquid that is extremely corrosive. It is mostly made in industrial settings by catalytically oxidizing ammonia and then absorbing it in water. Nitric acid’s content and purity are meticulously regulated to satisfy certain industrial needs.

Due to its reactive nature, industrial nitric acid must be manufactured, stored, and transported under strict safety and quality standards.

Key Applications of Industrial Nitric Acid

Industrial nitric acid supplied by SNDB is used across a wide range of sectors, including:

  • Fertilizer Industry: As a key raw material in the production of ammonium nitrate and other nitrogen-based fertilizers
  • Chemical Manufacturing: Used in the synthesis of dyes, intermediates, and specialty chemicals
  • Pharmaceuticals: Essential for producing active pharmaceutical ingredients and laboratory reagents
  • Metal Processing: Applied in metal pickling, etching, and surface treatment
  • Explosives and Mining: Used in the manufacturing of explosives and blasting agents

These diverse applications demand consistent quality, purity, and supply reliability—areas where SNDB excels.

SNDB’s Manufacturing Expertise

SNDB produces industrial-grade nitric acid that satisfies national and international requirements by utilizing cutting-edge manufacturing techniques and contemporary infrastructure. Every stage of manufacturing is overseen by qualified experts and strict quality control methods, from the selection of raw materials to the final shipping.

Key strengths of SNDB’s manufacturing expertise include:

  • Advanced production technology
  • Strict adherence to safety and environmental regulations
  • High-purity output suitable for demanding industrial applications
  • Scalable production capacity to meet bulk and customized requirements

Commitment to Quality and Safety

A key component of SNDB’s activities is quality and safety. To guarantee proper concentration, purity, and adherence to industry standards, every batch of nitric acid is put through extensive testing. In order to reduce risk and guarantee safe delivery to clients, SNDB also adheres to strict safety procedures throughout handling, storage, and transportation.

Reliable Supply and Global Export Capability

As a prominent nitric acid provider and exporter, SNDB serves both domestic and international markets. SNDB is able to deliver goods safely and on schedule in a variety of locations because to effective logistics, reliable packaging options, and adherence to international export regulations.

Whether supplying small quantities or bulk shipments, SNDB ensures uninterrupted supply and dependable customer support.

Why Choose SNDB for Industrial Nitric Acid?

Customers choose SNDB for its:

  • Proven industry experience
  • Consistent product quality
  • Reliable supply chain and timely delivery
  • Customer-focused approach
  • Strong reputation as a manufacturer, supplier, and exporter

A key component of many businesses, industrial nitric acid’s purity has a direct bearing on both operational effectiveness and safety. With strong scientific understanding, contemporary manufacturing capabilities, and a dedication to excellence, SNDB stands out as a trusted partner for industrial nitric acid solutions. Industries can obtain dependable goods supported by quality, safety, and worldwide reach by using SNDB.

SNDB as a Reliable Exporter of Acetic Acid to Global MarketsCategoriesUncategorized

SNDB – Best Exporter of Acetic Acid | Role of Acetic Acid in Organic Chemistry

Acetic acid is an important organic chemical used in many industries such as food, textiles, pharmaceuticals, plastics, and chemicals. Because of its wide industrial use, the demand for high-quality acetic acid is increasing worldwide. SNDB has become one of the leading manufacturers and exporters of acetic acid due to its high-quality production and global supply network.

About SNDB

SNDB is a well-known chemical manufacturing company in India that specializes in the production and export of acetic acid and other industrial chemicals. The company is known for its experience, modern manufacturing facilities, and strong focus on customer satisfaction. SNDB supplies acetic acid to both domestic and international markets.

Why SNDB is the Best Exporter of Acetic Acid

1. High Quality Production

SNDB follows strict quality control procedures to ensure that the acetic acid produced meets international standards. Each batch is tested for purity and safety before export.

2. Advanced Manufacturing Facilities

The company uses modern technology and advanced equipment for large-scale production of acetic acid, which ensures consistent quality and efficiency.

3. Global Export Network

SNDB exports acetic acid to many countries across Asia, the Middle East, and Africa through a strong distribution network and efficient supply chain system.

4. Wide Industrial Applications

Acetic acid supplied by SNDB is used in many industries such as:

  • Food industry (vinegar and preservatives)
  • Textile industry (dyeing and finishing)
  • Pharmaceutical industry (medicine production)
  • Chemical industry (esters, acetic anhydride, vinyl acetate)
  • Agriculture (pesticides and herbicides)

5. Customer Satisfaction and Packaging

SNDB provides acetic acid in different packaging options such as drums, bulk containers, and customized packaging according to customer needs. The company focuses on timely delivery and customer satisfaction.

6. Sustainable Production

SNDB uses eco-friendly and sustainable manufacturing methods to reduce environmental impact and maintain safety standards.

SNDB is considered one of the best exporters of acetic acid because of its high product quality, advanced manufacturing technology, global export network, and customer-focused approach. With increasing global demand for acetic acid, SNDB continues to play an important role in supplying high-quality acetic acid to industries around the world.

Nitric Acid: The Backbone of Fertilizer Industry| sndbCategoriesNitric Acid

Nitric Acid: The Backbone of Fertilizer Industry

Nitric Acid (HNO₃) is one of the most important industrial chemicals and plays a vital role in the fertilizer industry. It is a strong acid and powerful oxidizing agent used in the production of nitrogen-based fertilizers, which are essential for modern agriculture and global food production. Around 75–80% of nitric acid produced worldwide is used in fertilizers, which is why nitric acid is called the backbone of the fertilizer industry.

What is Nitric Acid?

Nitric acid is a colorless to yellowish, highly corrosive mineral acid with the chemical formula HNO₃. It is mainly produced from ammonia by a method called the Ostwald Process.

Basic Properties of Nitric Acid

  • Chemical Formula: HNO₃
  • Appearance: Colorless liquid
  • Nature: Strong acid
  • Highly corrosive and oxidizing agent
  • Used in fertilizers, explosives, dyes, plastics, and pharmaceuticals

Nitric Acid Production – Ostwald Process

Nitric acid is manufactured from ammonia in three main steps:

  1. Ammonia reacts with oxygen → Nitric Oxide (NO)
  2. Nitric Oxide reacts with oxygen → Nitrogen Dioxide (NO₂)
  3. Nitrogen Dioxide reacts with water → Nitric Acid (HNO₃)

This process is used in almost all nitric acid industries in the world.

Role of Nitric Acid in Fertilizer Industry

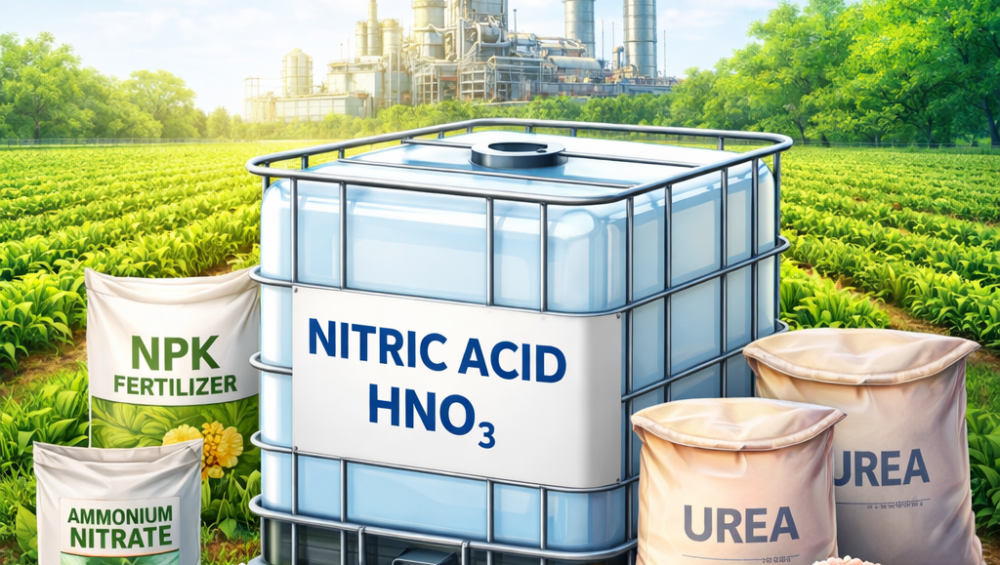
Nitric acid is mainly used to manufacture nitrogen fertilizers such as:

  • Ammonium Nitrate
  • Calcium Ammonium Nitrate (CAN)
  • Urea Ammonium Nitrate (UAN)
  • NPK Fertilizers
  • Potassium Nitrate

These fertilizers provide nitrogen, which is an essential nutrient for plant growth and increases crop yield and food production.

Why Nitric Acid is Called Backbone of Fertilizer Industry

Nitric acid is called the backbone of the fertilizer industry because:

  • It is the main raw material for nitrogen fertilizers.
  • About 80% of nitric acid is used in fertilizer production.
  • It helps convert ammonia into nitrate fertilizers.
  • It supports agriculture and food production.
  • Fertilizer industry depends heavily on nitric acid.

SNDB Chemicals – Manufacturer & Supplier (Nitric Acid)

SNDB Chemicals is a manufacturer and supplier of nitric acid in India, providing different concentrations such as 62% and 70% nitric acid for industrial use. The company supplies nitric acid in bulk packaging including HDPE carboys, drums, and IBC tanks, making it suitable for fertilizer, chemical, pharmaceutical, dye, and explosive industries. SNDB Chemicals focuses on quality control, safe handling, and timely delivery, which makes it a reliable supplier for small and large-scale industries. The company serves both domestic and industrial markets by supplying nitric acid as an important raw material used especially in fertilizer manufacturing, where nitric acid is required for producing ammonium nitrate and other nitrogen fertilizers.